Pinmi
Get a Quote
Pinmi
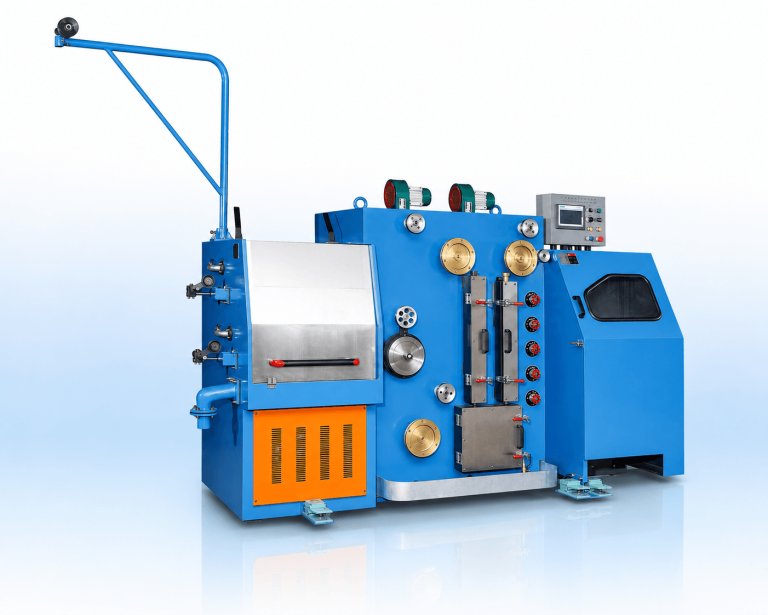
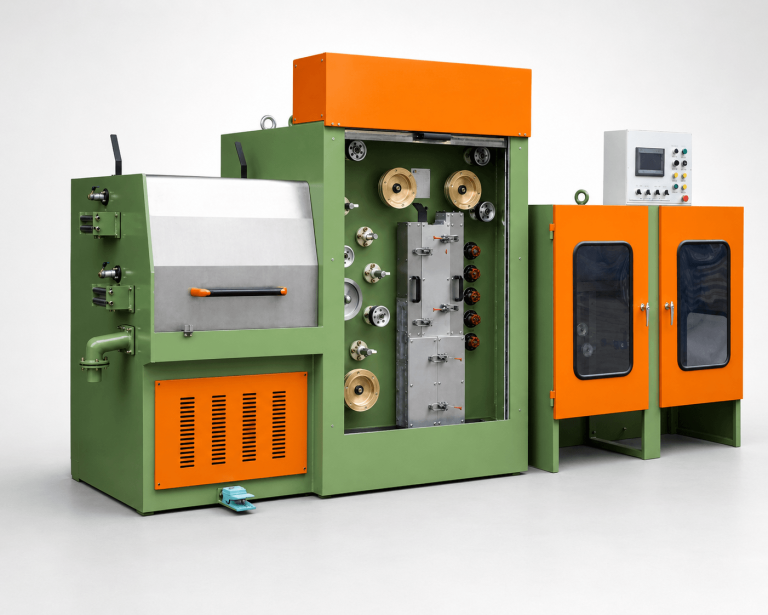
The machine can draw two wires simultaneously within the specified diameter range. This helps cable and conductor manufacturers increase intermediate wire output without adding a separate drawing line.
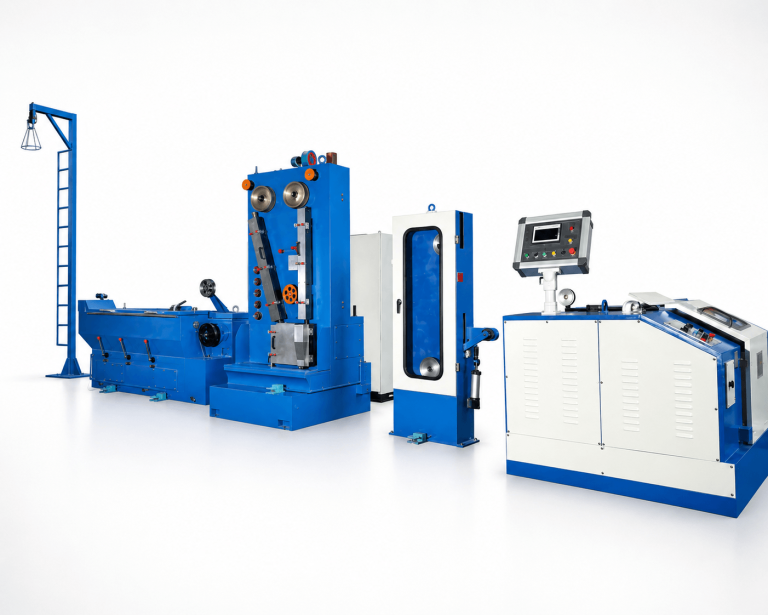
The SZ17B drawing unit and ST2000 annealer are combined in one production line, reducing intermediate handling and supporting continuous production of annealed soft copper wire.
Contact-type DC annealing, steam protection, cooling and compressed-air drying help improve wire softness, surface protection and elongation consistency.
Two K200 tension controllers use dancer and sensor feedback to coordinate take-up tension. This is important for reducing wire breakage and supporting stable high-speed production.
Full-submersible lubrication, tungsten carbide drawing rings, nickel alloy annealing rings and ceramic-treated sheaves help reduce wear and protect wire surface quality.

Power Cable Production

Electrical Wire Manufacturing

Copper Wire Processing

Aluminum Wire Production
Conductor Manufacturing
Non-Ferrous Metal Wire Plants
Fine Wire Preparation
The system is delivered as a sequence of coordinated stations, each built and tested in-house before shipment.

Basket pay‑off for stable wire feeding, ensures smooth wire entry for continuous dual‑wire production.

Max 17‑die intermediate drawing unit, tungsten‑carbide capstans, full‑submersible oil lubrication‑cooling system.

AC main motor with gearbox & belt transmission, supports high/low‑speed mode for different wire gauges.

Triangular short‑circuit online annealing unit with steam anti‑oxidation protection, completes copper wire softening.

Liquid cooling + compressed‑air drying, removes moisture before wire enters take‑up section.

Dancer‑roller tension feedback, synchronizes speed between annealer and spooler to lower wire breakage.

Pneumatic bobbin clamping & braking, independent traverse drive for neat wire‑laying.

Siemens S7‑1200 PLC + touch‑screen HMI, frequency‑conversion control, data display and full‑fault alarm.
Reference size cover most projects. Intermediate capacities and custom configurations are engineered on request.
| Item | Specification |
| Machine Model | SZ17B/ST2000/K200/K200/S630/S630 dual wire intermediate drawing machine with annealer and single spoolers |
| Main Line Configuration | SZ17B drawing unit 1 set; ST2000 annealer 1 set; K200 tension controller 2 sets; S630 single spooler 2 sets; electrical control system 1 set |
| Raw Material | Low-oxygen or oxygen-free round copper wire: 1.35 mm, 1.71 mm, 2.52 mm; aluminum wire configuration is customized according to project requirements |
| Maximum Inlet Wire Diameter | 3.50 mm |
| Finished Wire Diameter | Dual wire: 2 x 0.30-1.12 mm; single wire: 1 x 0.30-1.60 mm |
| Maximum Mechanical Speed | 1800 m/min |
| Typical Production Speed | 2 x 0.30 mm: 25 m/s; 2 x 0.40 mm: 24 m/s; 2 x 0.60 mm: 23 m/s; 2 x 0.80 mm: 20 m/s; 2 x 1.04 mm: 18 m/s; 2 x 1.12 mm: 16 m/s; 1 x 1.60 mm: 15 m/s |
| Annealed Wire Elongation | 23%-28% for 0.30-0.40 mm; 25%-31% for 0.60-1.60 mm according to source table |
| Number of Drawing Dies | Maximum 17 dies |
| Drawing Die Outer Diameter | 25 mm |
| Mechanical Elongation | Last die 13.38%; No. 1-16 dies 18.18% |
| Drawing Cone Diameter | Maximum 250 mm |
| Capstan Diameter | 250 mm |
| Main Drawing Motor | AC 90 kW inverter motor, Innomotics / Siemens brand |
| Drawing Unit Net Weight | About 4260 kg including motor |
| Whole Line Weight | About 14000 kg |
| Total Machine Capacity | 375 kVA |
| Annealer Model | ST2000 contact-type triangular short-circuit DC annealer |
| Annealing Wire Diameter | Dual wire: 2 x 0.30-1.12 mm; single wire: 1 x 0.30-1.60 mm |
| Rated Annealing Current | Maximum 2000 A DC |
| Annealing Voltage | Maximum 60 V DC |
| Annealing Capacity | 193 kVA |
| Steam Generator Installed Power | 12 kW |
| Steam Quantity | 12 kg/h |
| Annealer Size | 1500 x 1750 x 2850 mm |
| Annealer Net Weight | 3000 kg |
| Tension Controller | K200 tension controller, 2 sets |
| Tension Controller Size / Weight | 1000 x 410 x 1900 mm; about 250 kg |
| Spooler Model | S630 high-speed single spooler, 2 sets |
| Take-up Range | Dual wire: 2 x 0.30-1.12 mm; single wire: 1 x 0.30-1.60 mm |
| Spooler Mechanical Speed | Maximum 1800 m/min |
| Take-up Motor Power | AC 11 kW |
| Traverse Motor Power | 1 kW |
| Positioning Motor Power | 9 W |
| Suitable Spool | 630 / 500 mm bobbins; bobbin size can be customized after confirmation |
| Spool Capacity | Maximum 500 kg |
| Brake Method | Pneumatic |
| Spooler Size / Weight | 2450 x 1650 x 1460 mm; 2150 kg |
| Lubrication Method | Full-submersible drawing oil lubrication and cooling; external tank, filtration and heat exchanger or cooling tower are prepared according to project scope |
| Drawing Lubricant Requirement | Working pressure 0.20-0.40 MPa; temperature <=30 deg C; flow 18-26 m3/h |
| Annealer Compressed Air | 0.6-0.7 MPa, fluctuation +/-0.02 MPa, dew point -25 deg C, 300 L/min |
| Annealer Water Supply | 0.2-0.4 MPa, 25 deg C, pH 7-8, 500 L/min; water hardness max. 5 dH for steam generator and max. 12 dH for cooling liquid |
| Spooler Compressed Air | 0.6-0.7 MPa, fluctuation +/-0.02 MPa, dew point -25 deg C, 50 L/min |
| Power Supply | 3 x 380 VAC (-5% to +10%), single phase 220 V (-5% to +10%), 50 Hz (+/-2%) |
| Control System | AC inverter control; Siemens S7-1200 PLC; KTP700 / MTP1200 touch screen according to supplied configuration |
| Main Electrical Brands | Yaskawa inverters; Siemens PLC and low-voltage switches; NSK bearings; tungsten carbide drawing cone and capstan rings; nickel alloy annealing conduction rings; ceramic-treated sheaves; Habasit flat belt |
| Operation Direction | Right operation direction: wire inlet on the left side and take-up on the right side when the operator faces the drawing machine |
| Color | Mechanical part RAL5015 blue; electrical cabinet RAL7035 gray |
| Customization Available | Copper or aluminum wire process, inlet and outlet wire size, die schedule, annealer configuration, spool size, take-up method, electrical brand, voltage, layout and auxiliary cooling/filtering system |
Reference values — final parameters are confirmed during process design based on raw material, site conditions and product standard. Replace with your confirmed datasheet values before publishing.
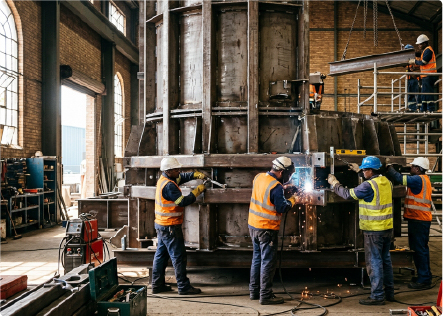
workshop
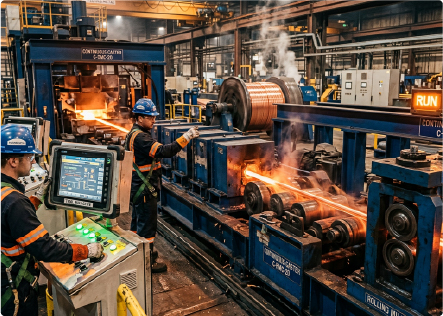
trial run
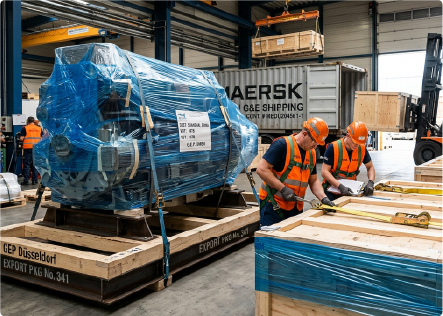
container load
workshop
Share your capacity, raw material and site conditions — we'll come back with a process route, equipment selection and a turnkey path to production.


No.310–311 National Road, Quanshan District, Xuzhou City, China
Check our FAQs below, or reach out to our team for tailored answers and project quotation.
Get a Quote