Pinmi
Get a Quote
Pinmi
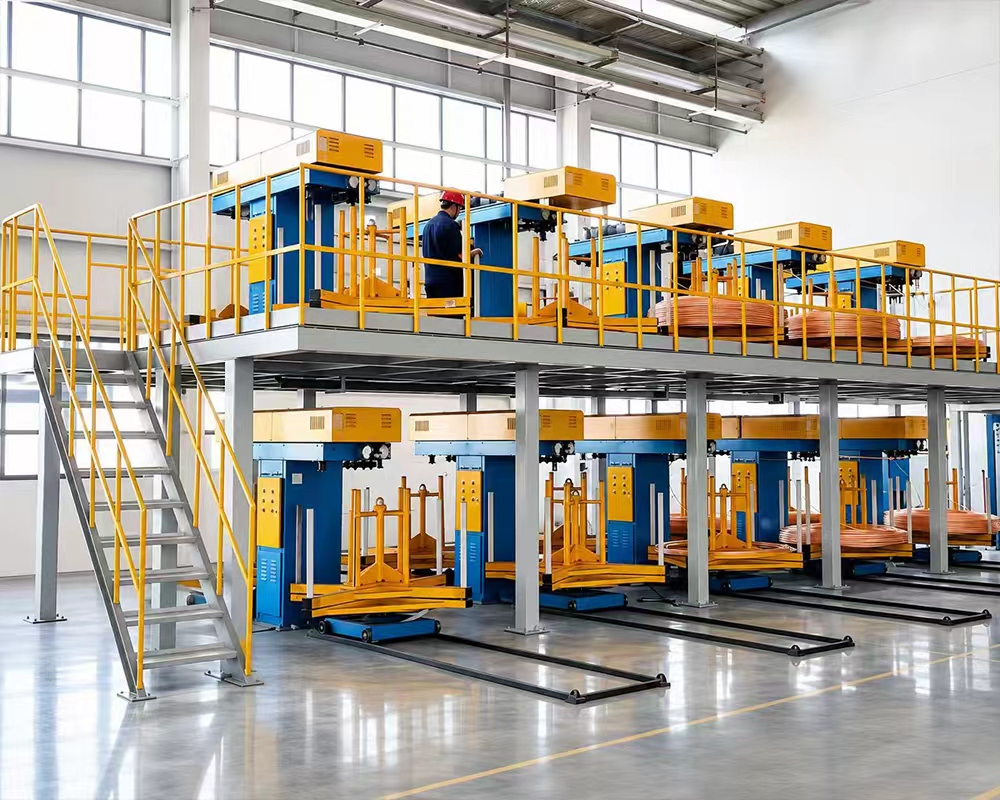
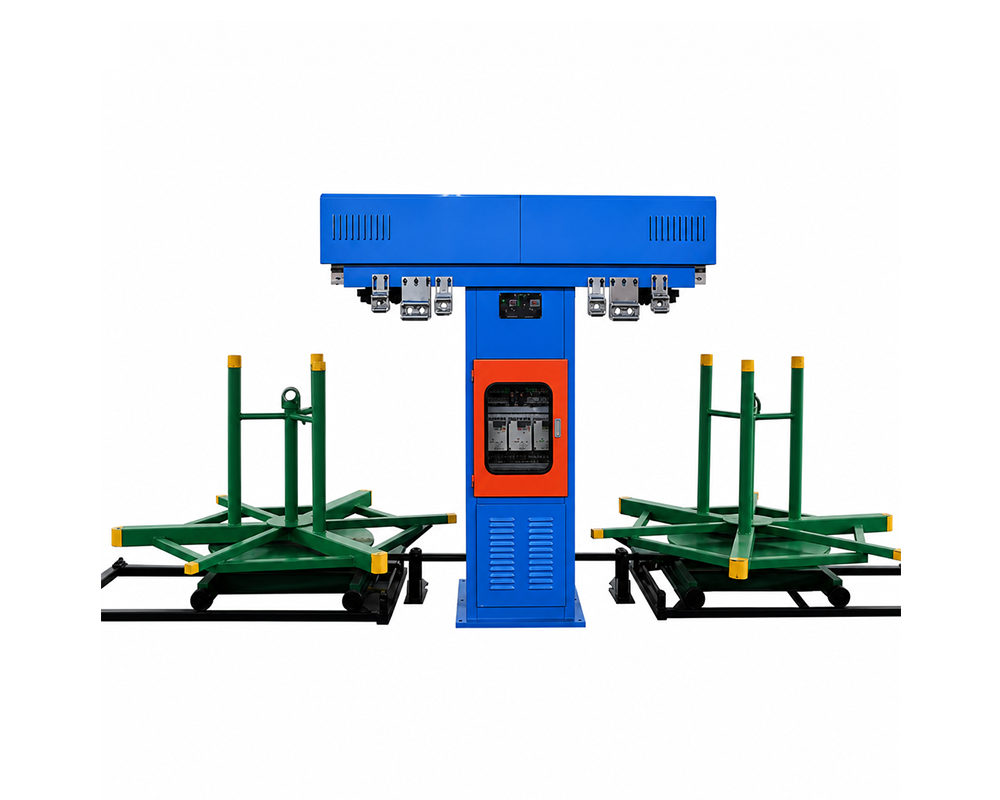
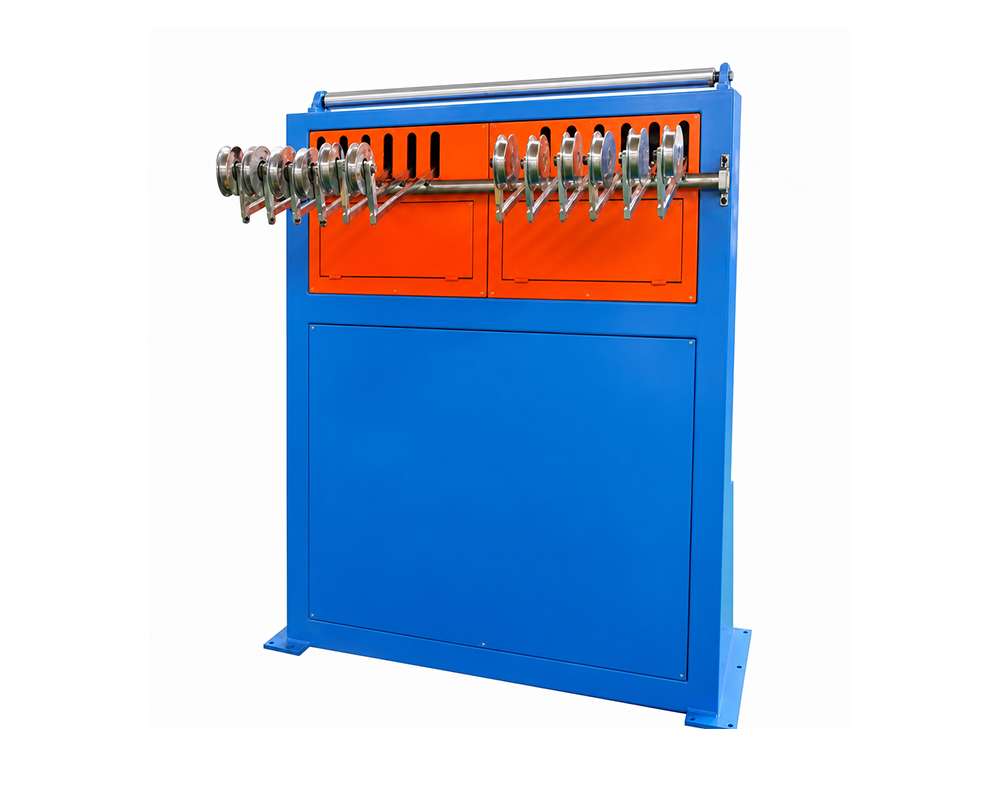
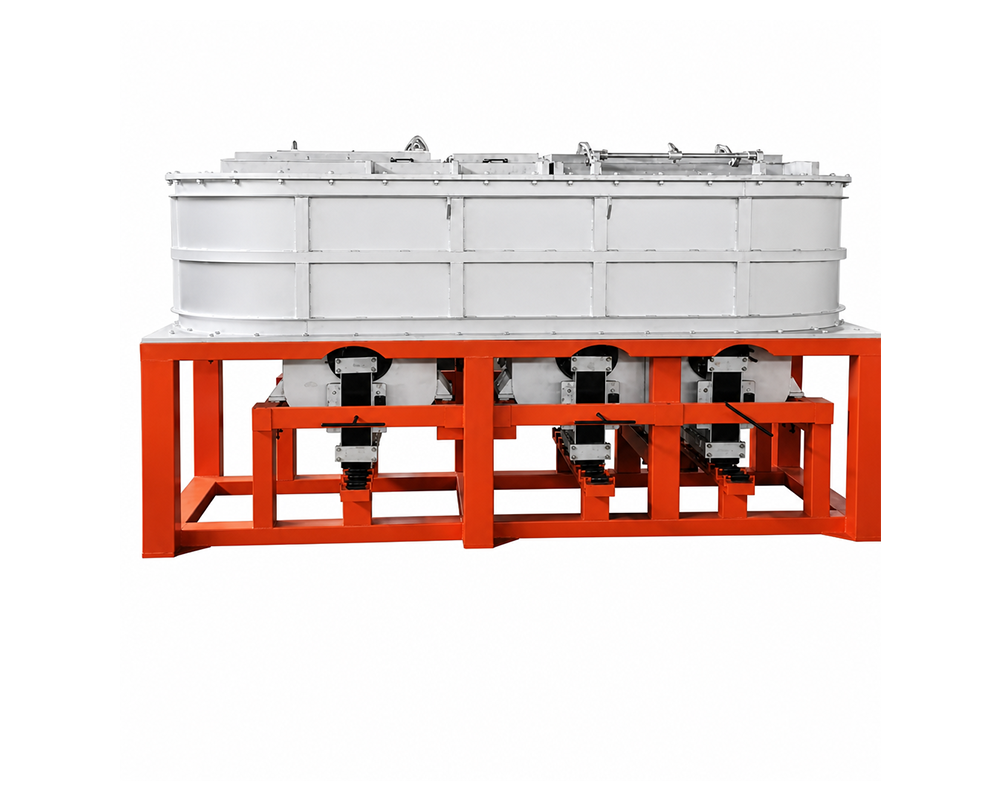
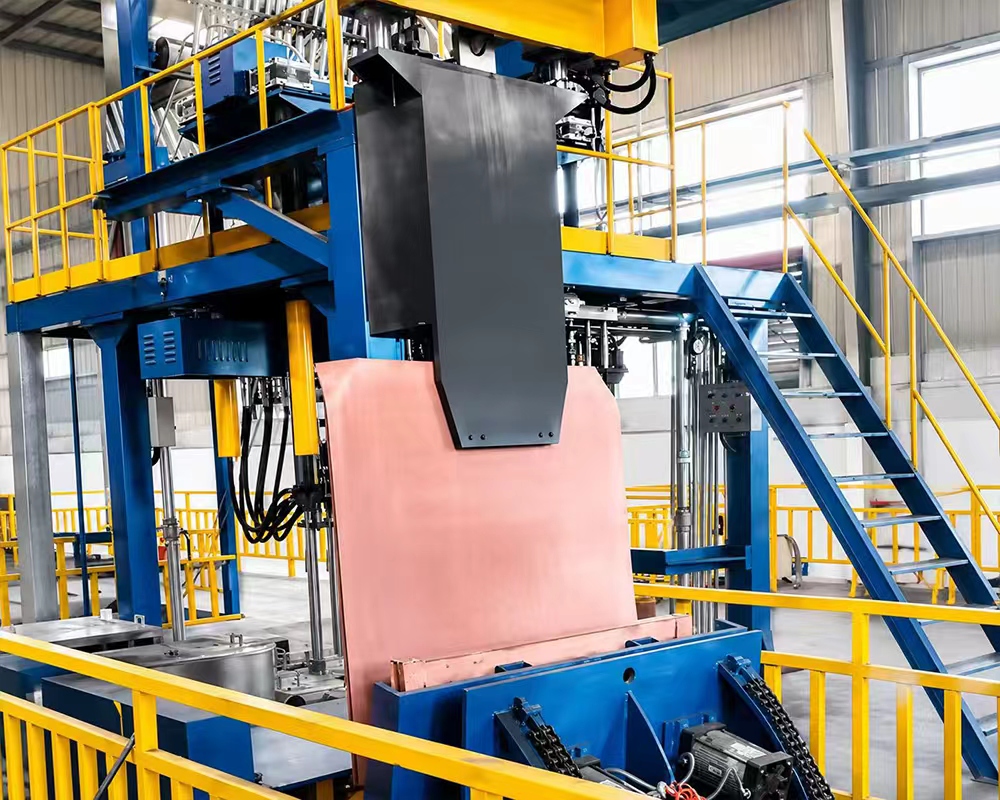
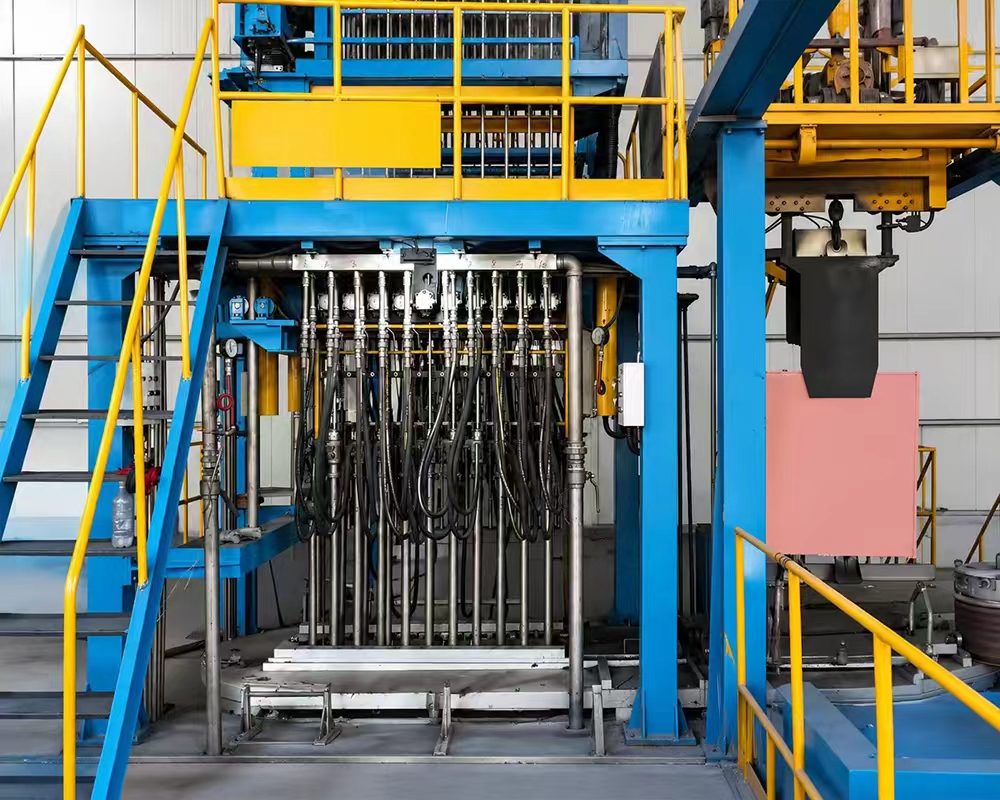
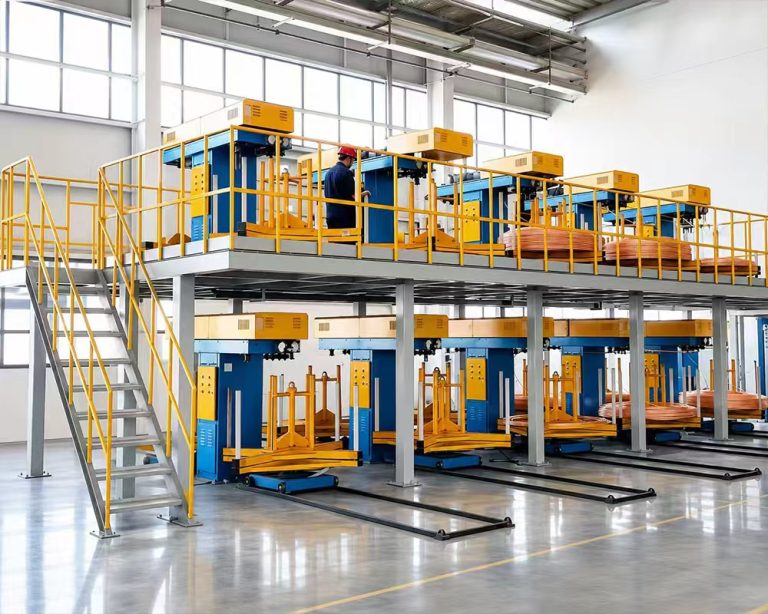
The machine casts oxygen-free copper rod directly from molten copper through crystallizers, supporting continuous production and reducing intermediate handling.
The SL28 configuration can upcast 28 rods at the same time. Four servo systems drive the traction mechanism, with each servo system pulling seven rods.
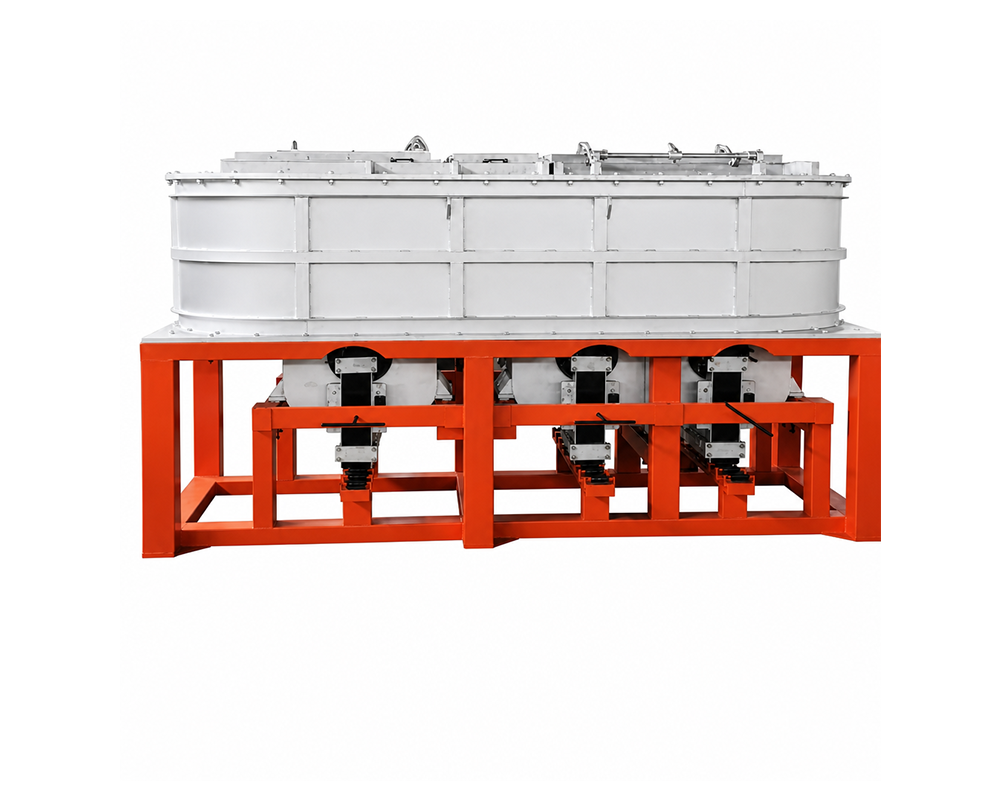
The furnace includes two melting chambers, one transition chamber and one holding chamber. This structure supports stable molten copper supply and steady holding temperature.
The documented finished rod target includes oxygen content <=10 ppm and soft-state resistivity <=0.01724 ohm mm2/m, supporting high-conductivity electrical applications.
Upcasting speed, pitch, reverse amount and pause time can be set through PLC and touch screen. This helps match different rod diameters and casting conditions.

Wire and Cable Manufacturing

Electrical Material Production

Electronic Copper Material

Copper Wire Drawing Plants
Non-Ferrous Metal Processing Plants
OFC Copper Rod Production Projects
The system is delivered as a sequence of coordinated stations, each built and tested in-house before shipment.

Continuous gas-fired smelting of cathode or clean scrap, with staged combustion for low oxygen pickup.

Temperature stabilization and buffer capacity between smelting and casting, 5–20 T depending on line size.

Wheel-and-belt continuous casting producing a uniform trapezoidal bar for the rolling mill.

10–14 stands reducing the cast bar to Ø 8 mm rod with tight dimensional tolerance.

In-line cooling, surface reduction and wax coating for oxidation protection.

Basket coiling of finished rod, typically 4–5 T coils, ready for strapping and dispatch.

PLC line control, drives, HMI and data logging — one control architecture for the whole line.

Baghouse dust collection sized to the furnace, engineered to local emission standards.
Reference sizes cover most projects. Intermediate capacities and custom configurations are engineered on request.
| Equipment | Function |
| QW4B Power-Frequency Induction Combined Furnace | Melts cathode copper, transfers molten copper through transition chamber and stabilizes molten copper in the holding chamber. |
| Induction Furnace Electrical Control System | Controls voltage regulation, compensation, balancing, power monitoring, furnace temperature and safety alarms. |
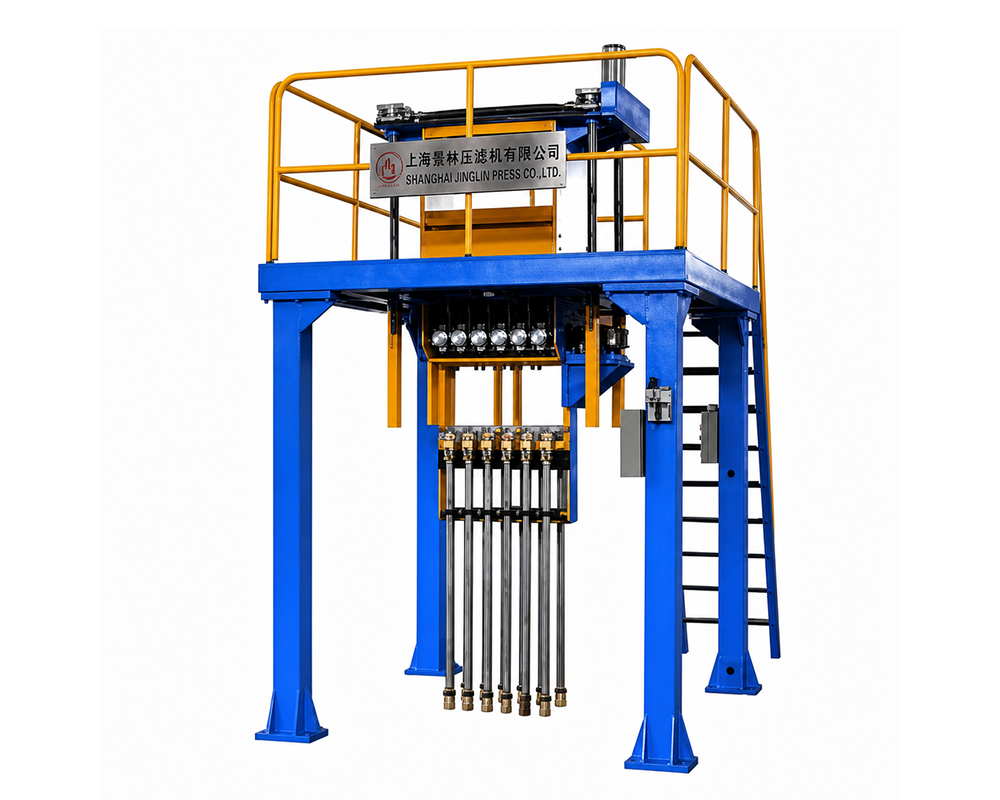
| 28-Head Upcasting Machine | Uses servo traction, crystallizers, lifting mechanism and liquid level tracking to continuously cast copper rods upward. |
| Graphite Crystallizers | Rapidly cool and crystallize molten copper into solid rods. Each crystallizer can be replaced separately. |
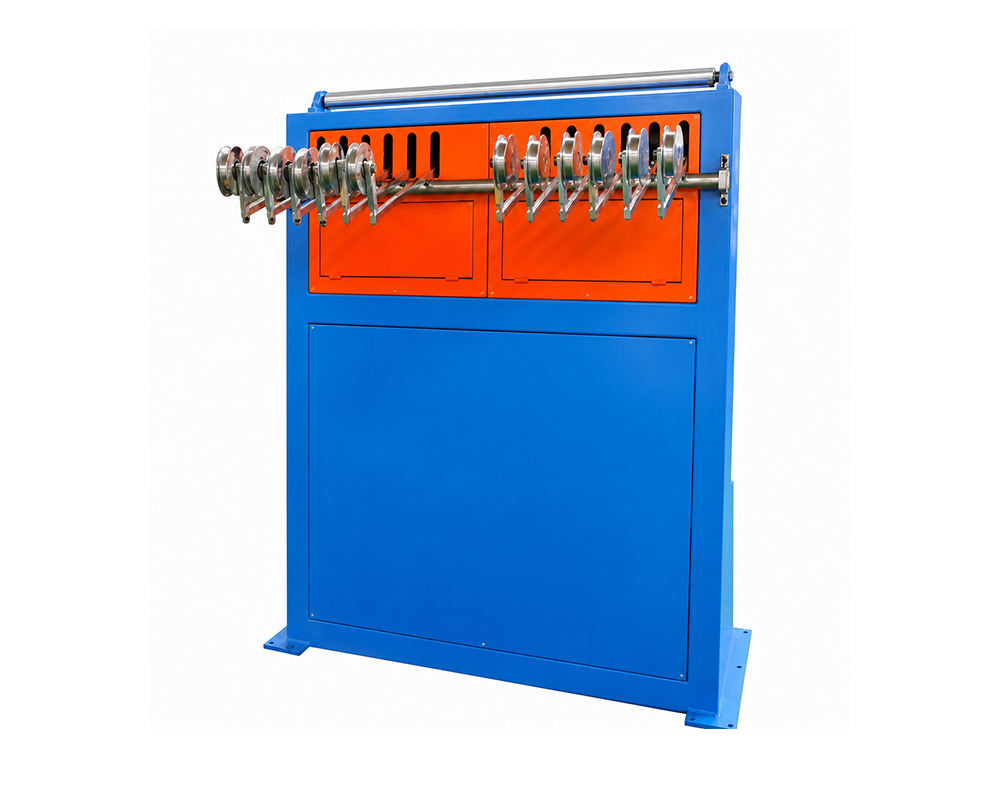
| Guide Wheel Frame | Guides upcast copper rods smoothly toward each coiler and prevents interference between rods. |
| Intermediate Support Frame | Supports rods between guide frame and limiting device, keeping rod paths stable and separated. |
| 14-Head Synchronous Limiting Devices | Coordinate upcasting speed and coiling speed through tension swing arms and signal feedback. |
| Double-Head Coilers | Fourteen coilers collect up to 28 rod coils with PLC-controlled automatic tracking and laying. |
| Cantilever Electric Feeding Devices | Lift and feed whole cathode copper plates into melting chambers from both sides of the furnace. |
| Cooling Water System | Supplies independent cooling water circuits for crystallizers, induction coils and water jackets with pressure, temperature and flow monitoring. |
| Temperature Measurement System | Measures molten copper temperature, cooling water inlet/outlet temperature and return-water flow for process monitoring. |
| Electrical Control System | Integrates furnace control, upcasting control, coiler control and cooling water control into a coordinated production system. |
Reference values — final parameters are confirmed during process design based on raw material, site conditions and product standard. Replace with your confirmed datasheet values before publishing.
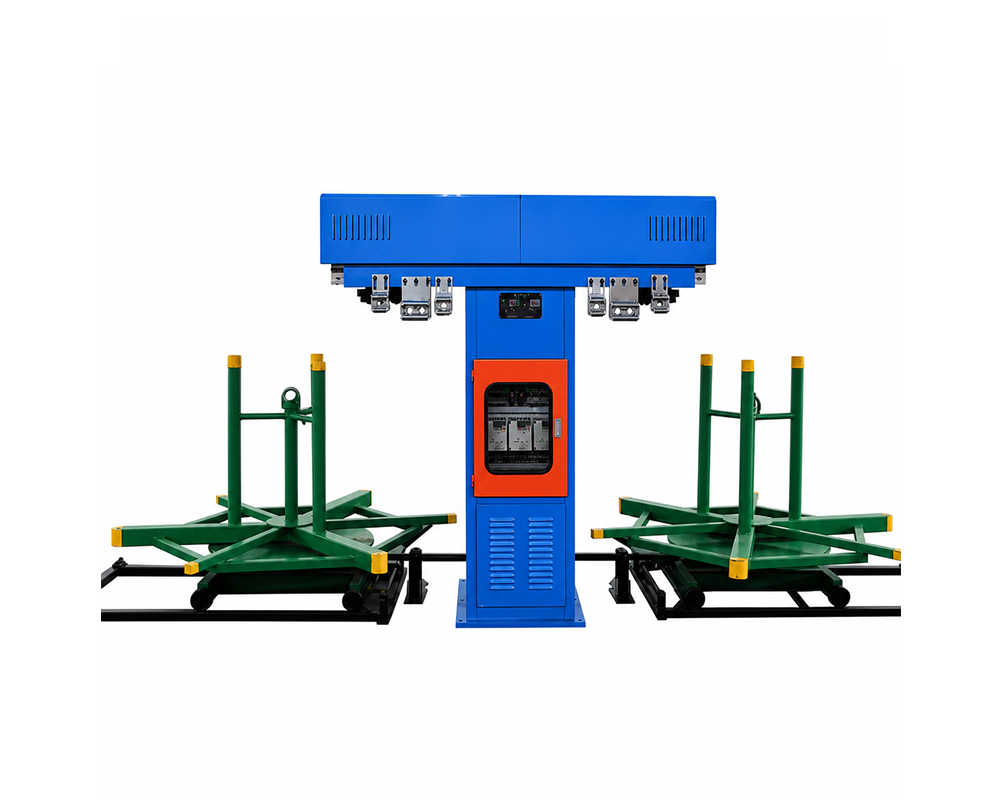
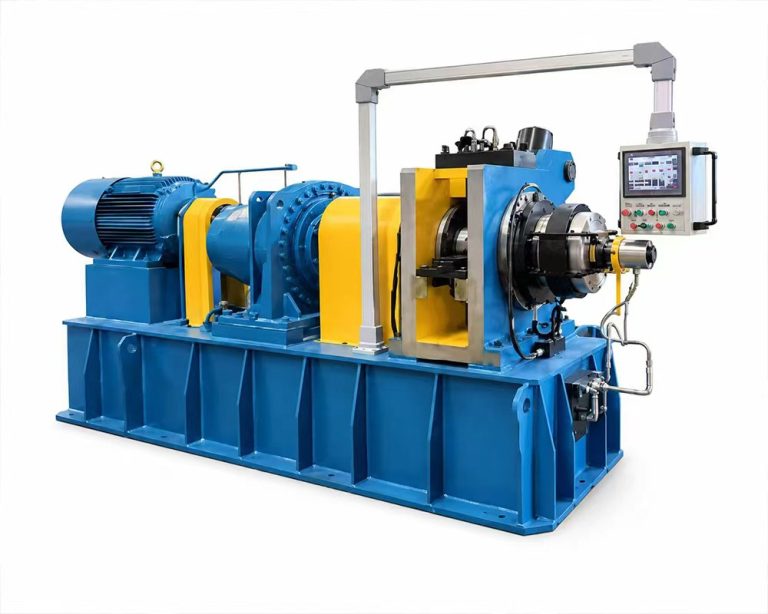
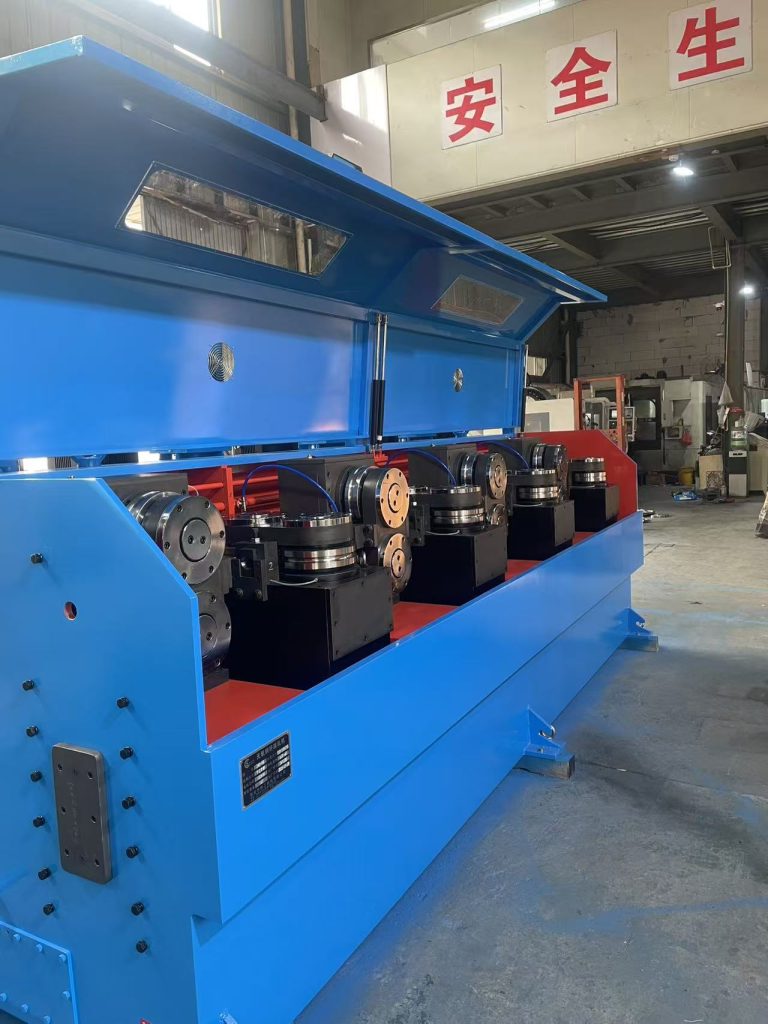
Actual photos
Actual photos
Actual photos
Actual photos
Share your capacity, raw material and site conditions — we'll come back with a process route, equipment selection and a turnkey path to production.


No.310–311 National Road, Quanshan District, Xuzhou City, China
Check our FAQs below, or reach out to our team for tailored answers and project quotation.
Get a Quote