Pinmi
Get a Quote
Pinmi
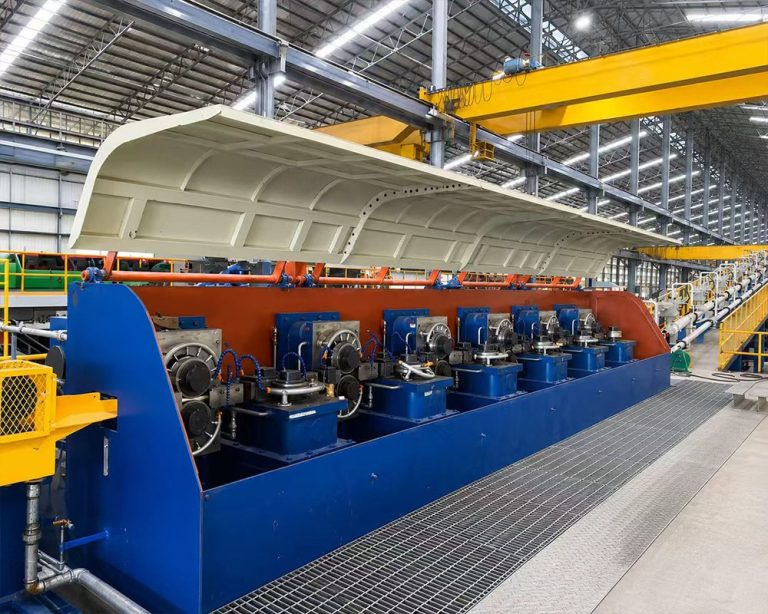
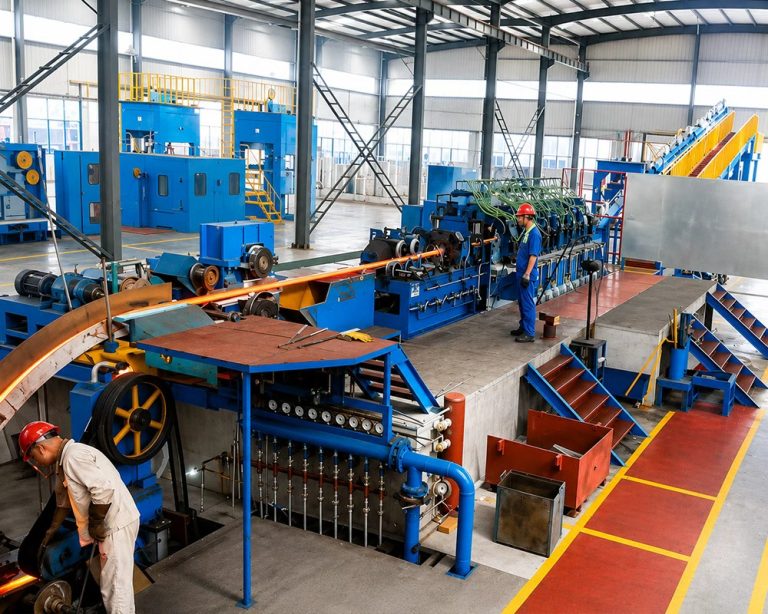
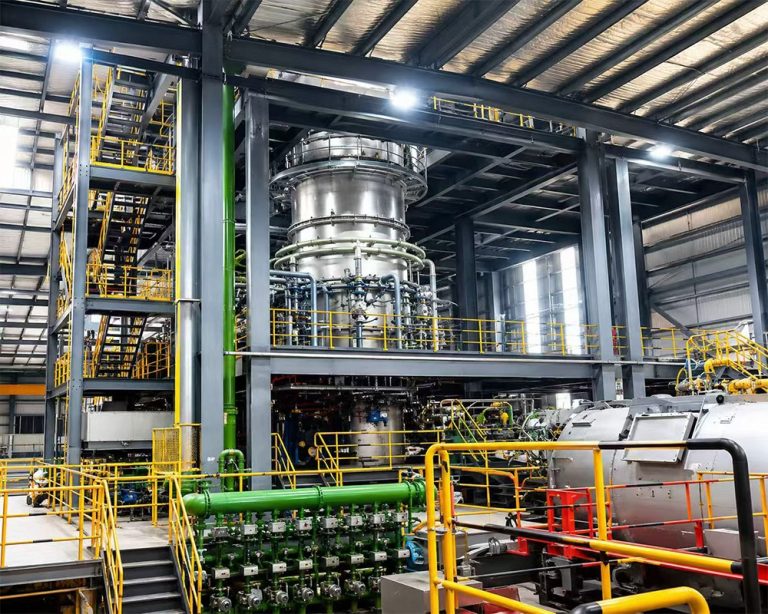
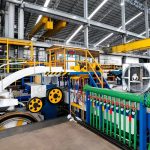
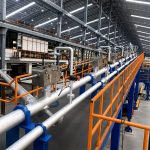
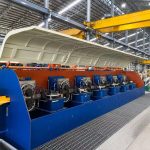
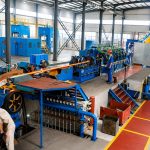
Complete copper CCR line covering copper melting, continuous casting, rolling and take‑up procedures.
High‑capacity shaft furnace to deliver stable molten copper supply for mass production.
Maintains stable liquid‑level and temperature to guarantee steady continuous‑casting operation.
Adopts 2100 mm crystallization wheel with 3800 mm² billet cross‑section.
Features HMI, sensors, CCTV monitoring and UPS backup for copper‑flow control under power failure.
Integrated roughing and finishing stands for uninterrupted copper‑rod rolling.

Copper rod production plants

Wire and cable manufacturing

Electrical conductor production

Power cable material production
Copper processing factories
Non-ferrous metal processing projects
Complete copper CCR production line projects
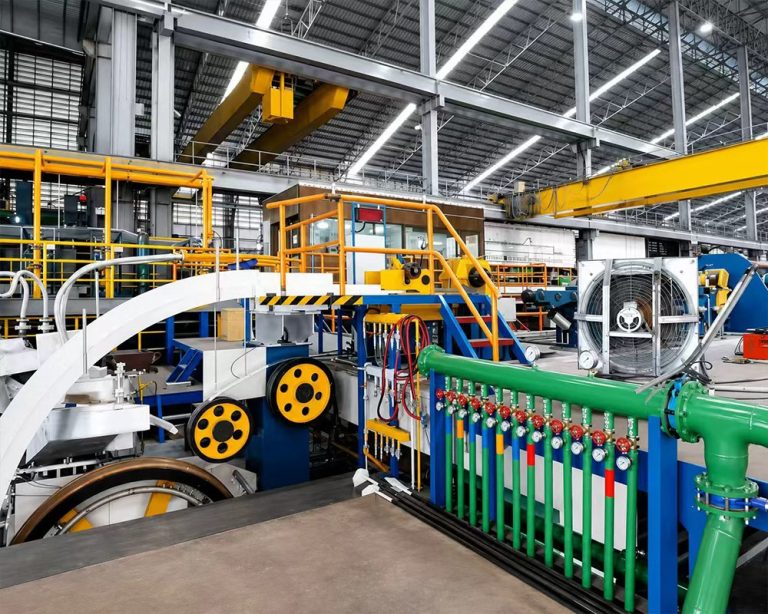
The system is delivered as a sequence of coordinated stations, each built and tested in-house before shipment.

25T/H shaft melting furnace with feeding system, CCTV monitoring and emergency braking for high‑capacity copper melting.

Tilting‑type holding furnace with combustion unit, refractory lining for stable molten‑copper temperature & level.

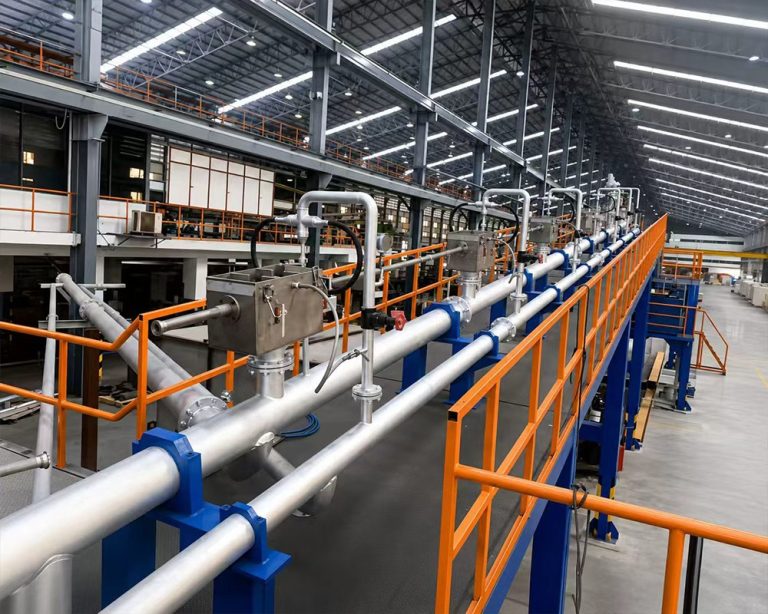
Complete launder shell, burners, slag‑removal trough and refractory lining for smooth molten copper transfer.

HMI, CCTV sensors & UPS backup, realizing closed‑loop automatic copper‑flow casting control.

Equipped with 2100 mm crystallization wheel for casting copper billet of 3800 mm² cross‑section area.

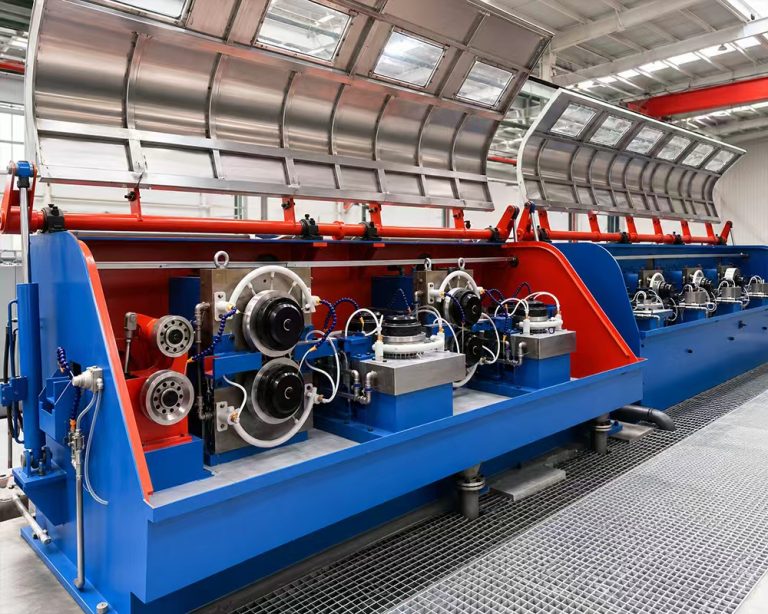
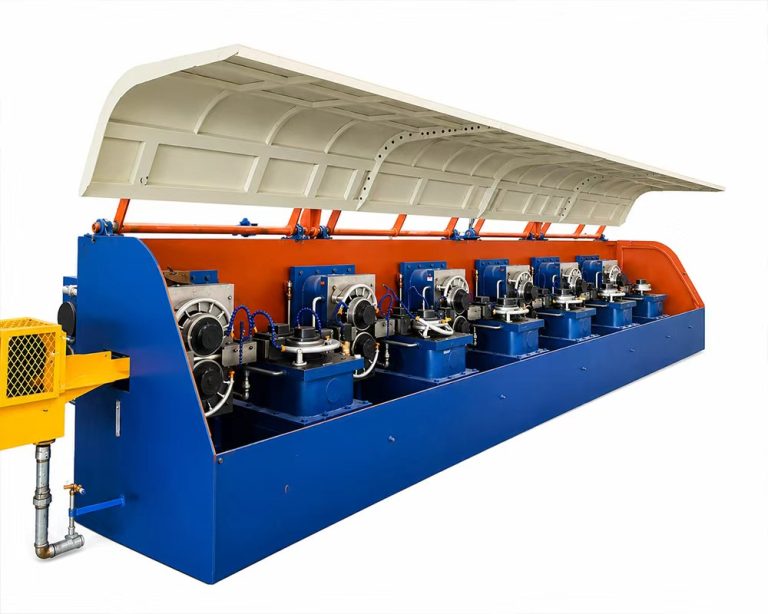
Full 2‑roller mill with 4 roughing & 8 finishing stands for continuous copper‑rod rolling.

Rear traction, winding, receiving & compaction functions for finished copper rod collection.

Redundant‑pump emulsion, gear‑oil and take‑up cooling system with multi‑parameter monitoring.
Reference sizes cover most projects. Intermediate capacities and custom configurations are engineered on request.
|
System |
Main Configuration |
|
Melting System |
25T/H shaft melting furnace, feeding system, tilting trolley, hopper, 45 kW charging drive motor, CCTV monitoring, emergency braking system. |
|
Holding Furnace |
16T holding furnace with tilting mechanism, hydraulic power unit, combustion equipment, refractory lining and real-time data display. |
|
Launder System |
Launder steel shell and covers, launder burners, slag removal trough, gas distribution tanks, metal hoses, refractory lining and lower launder mobile mechanism. |
|
Automatic Casting System |
Programmable control system, CCTV camera system, video sensors, automatic measuring and actuation components, holding furnace level sensor, touchscreen HMI and UPS protection. |
|
Casting Machine |
Six-wheel casting machine with 3800 mm2 billet cross-sectional area, 2100 mm crystallization wheel, 7.5 kW AC variable-frequency drive motor and 1.5 kW servo stopper control motor. |
|
Front Traction |
Front traction machine with 7.5 kW AC motor. |
|
Rolling Shear |
Rolling shear machine with 30 kW AC motor and 120 W brake motor. |
|
Pre-Straightening |
Pre-straightening machine with four 0.75 kW brushing motors. |
|
Mobile Hydraulic Shear |
Mobile hydraulic shear for auxiliary cutting and handling in the CCR line. |
|
Continuous Rolling Mill |
Full 2-roller continuous mill with 4 roughing stands and 8 finishing stands. Rolling motors include 37 kW, 45 kW, 55 kW, 75 kW and 90 kW AC motors with encoders according to stand position. |
|
Cooling and Reducing Take-Up |
Hydraulic take-up device with rear approach bridge, rear traction machine, rod winding mechanism, material receiving machine, hydraulic system, conveyor rollers, compactor and wax liquid pump. |
|
Emulsion Lubrication |
Hoffman vacuum paper belt filter, high-pressure emulsion pumps, emulsion lift pump liquid level controller, 120 m2 plate heat exchanger, more than 60 m3 emulsion tank and monitoring transmitters. |
|
Gearbox Lubrication |
Gear oil pumps, GLQ-100 filters, 8 m3 oil tank, 40 m2 plate heat exchanger, oil temperature transmitter and oil pressure transmitter. |
|
Take-Up Cooling |
Cooling pumps, 160 m2 plate heat exchanger, cooling liquid temperature below 35 deg C, 100 m3/h cooling liquid consumption, pressure above 0.4 MPa and more than 80 m3 cleaning liquid tank. |
|
Electrical Control |
Power switch cabinet, drive cabinet, auxiliary machine cabinet, relay control cabinet, casting console, main console, rod take-up console, industrial computer, Siemens G120 VFDs, Siemens S7-1200 PLC and 12-inch color HMI touchscreens. |
| Molten aluminum temperature | 700-850 deg C |
| Furnace pressure | 30-50 Pa |
| Lining structure | Full castable refractory lining |
| Lining service life | >=5 years, excluding wearing areas such as door opening and outlet |
| Furnace wall temperature | <= ambient temperature +55 deg C, excluding thermal bridge points |
| Molten bath depth | 525 mm |
| Drossing slope angle | 30 degrees |
| Furnace door opening | 1500 x 1500 mm |
| Door lifting method | Hydraulic cylinder + chain wheel set |
| Door compression method | Double-side pneumatic cylinder compression |
| Outlet structure | Concentric rotary outlet |
| Molten aluminum casting flow rate | >=10 t/h |
| Control system | Siemens S7-1500 PLC + 12-inch touch screen |
| Noise | <=85 dB measured 1.5 m from equipment |
Reference values — final parameters are confirmed during process design based on raw material, site conditions and product standard. Replace with your confirmed datasheet values before publishing.
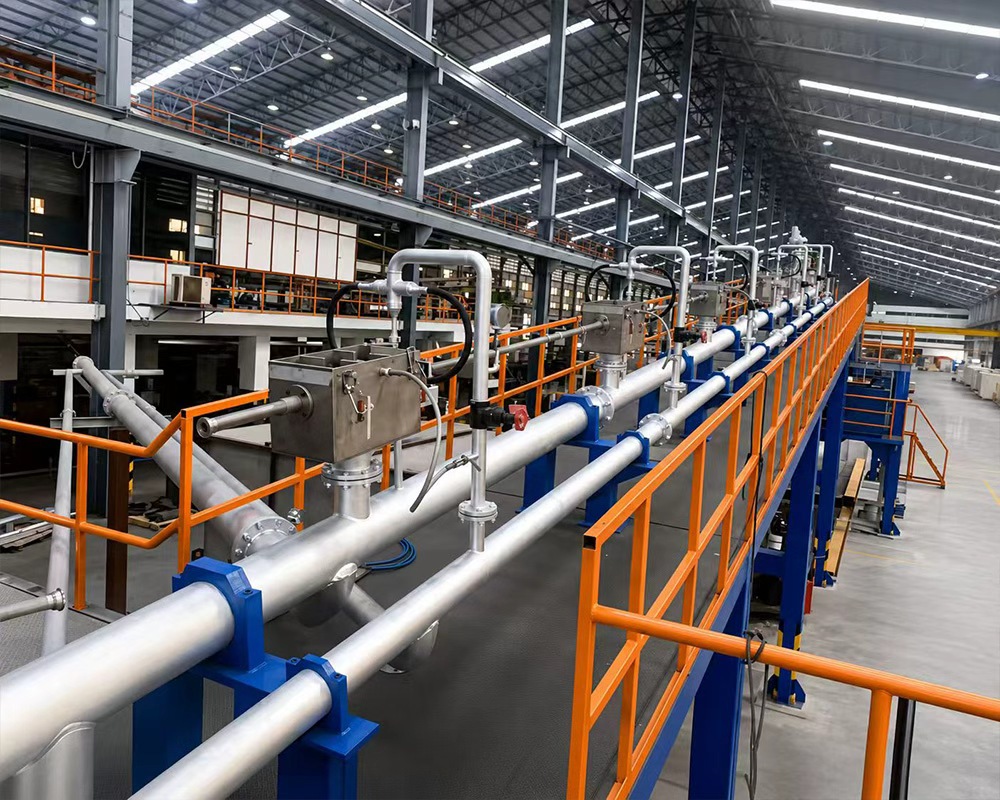
workshop
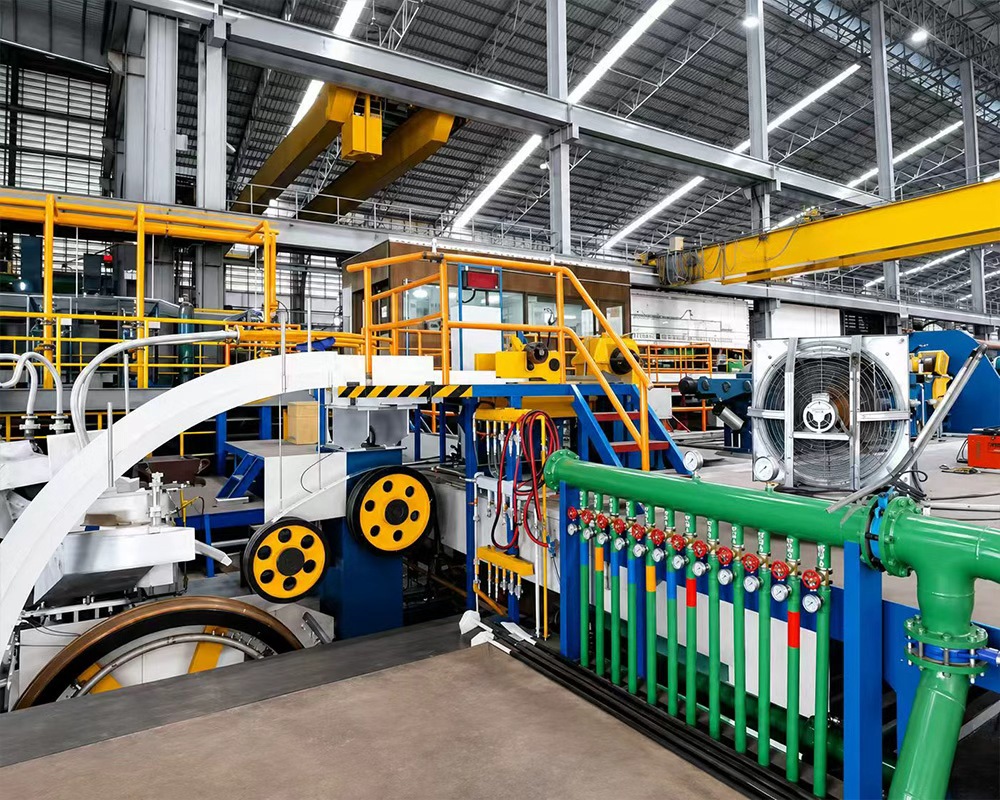
trial run
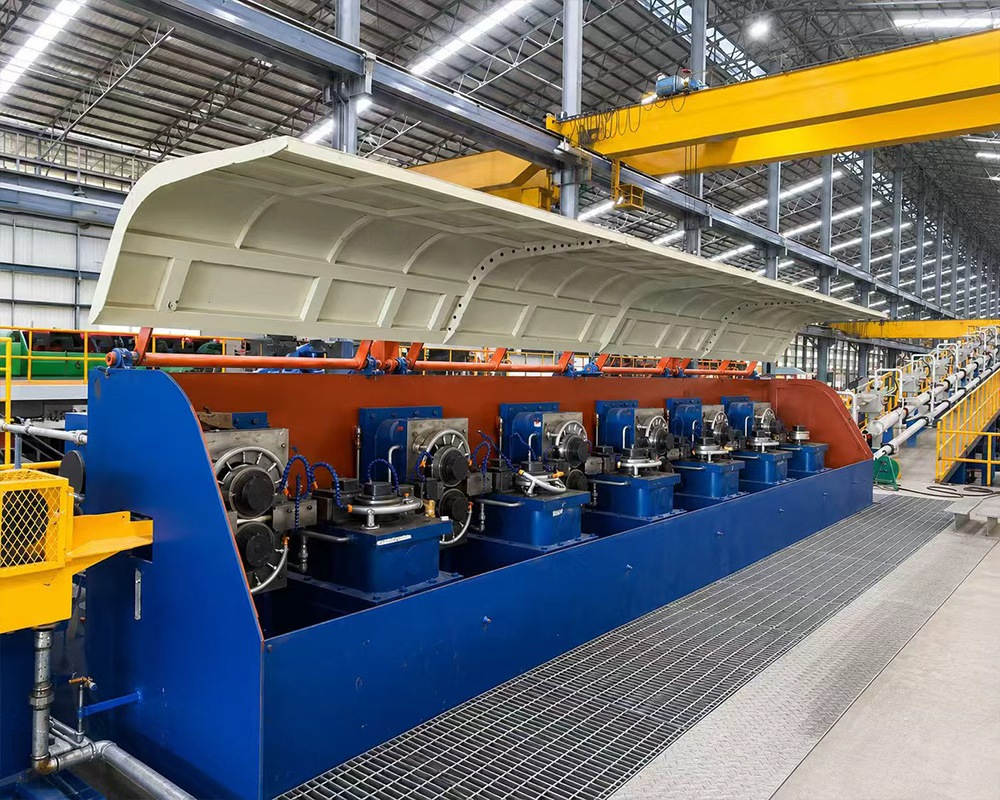
container load
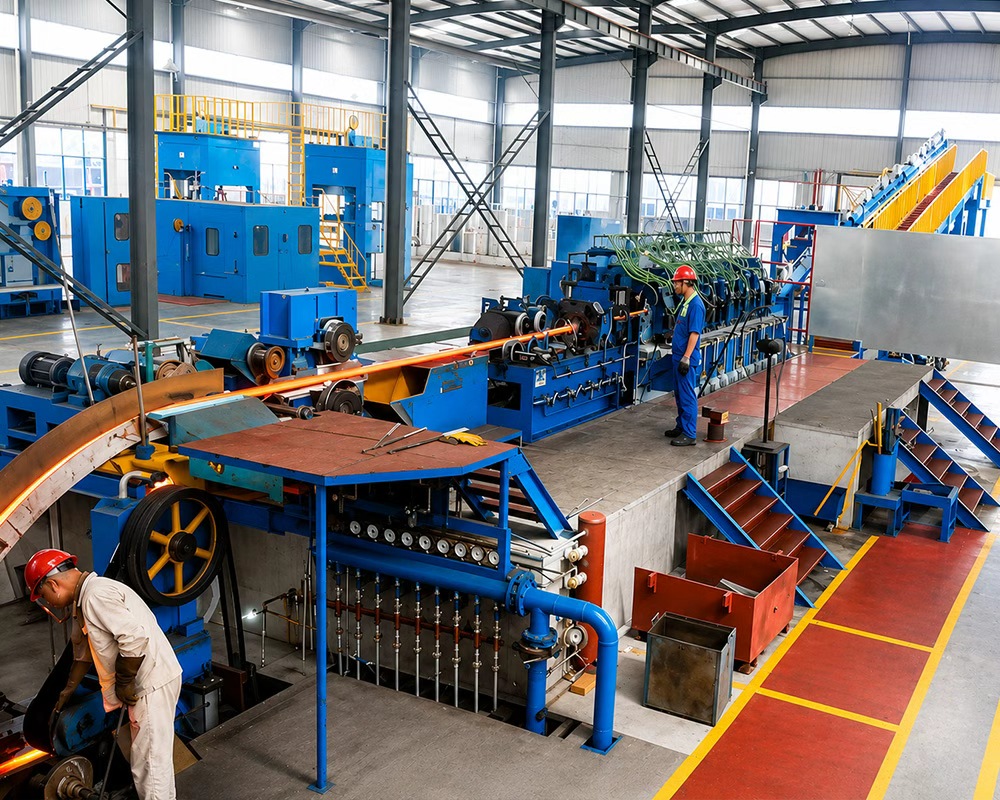
workshop
Share your capacity, raw material and site conditions — we'll come back with a process route, equipment selection and a turnkey path to production.


No.310–311 National Road, Quanshan District, Xuzhou City, China