Pinmi
Get a Quote
Pinmi
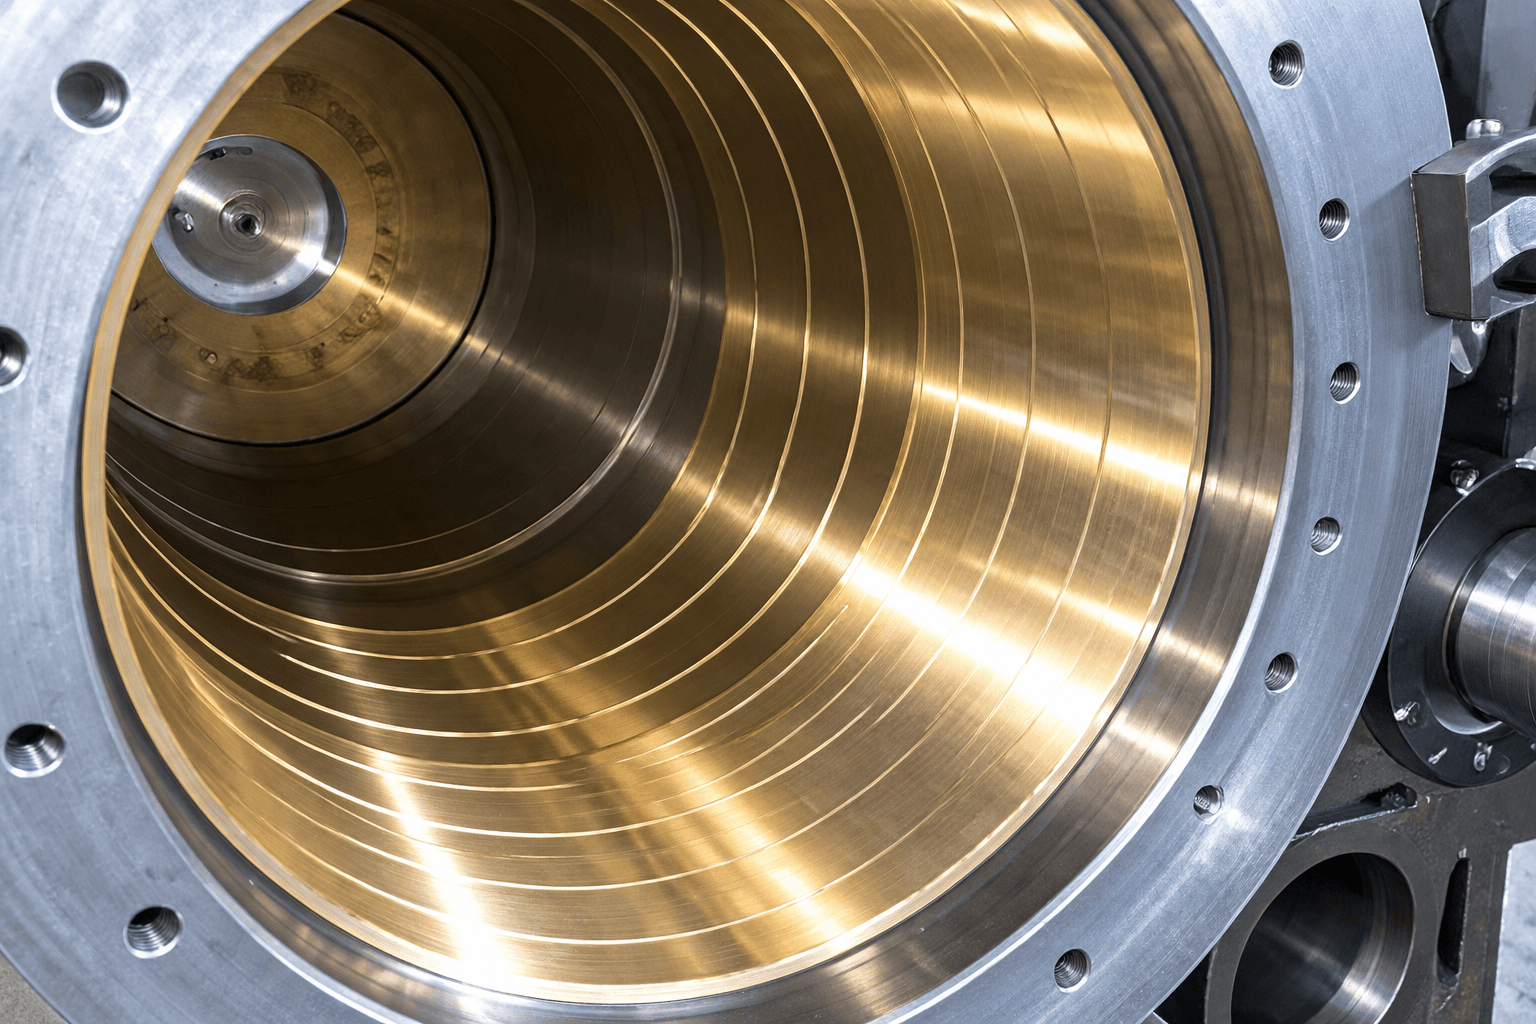
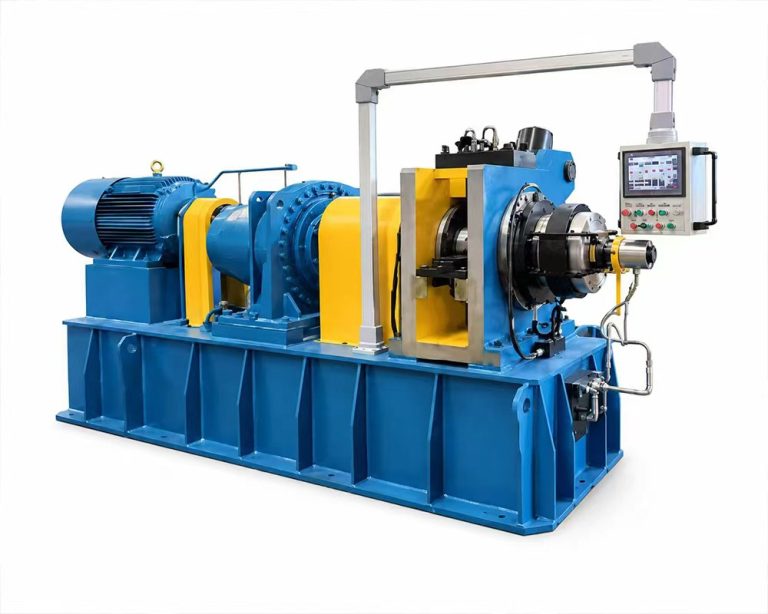
The machine accommodates billet diameters of Φ250–300 mm, with an extrusion container inner diameter of Φ260–315 mm. For seamless tube production, the reference processing range includes outer diameters from Φ60 mm to Φ200 mm, inner diameters from Φ50 mm to Φ150 mm and wall thicknesses of 5 mm or greater.
Its double-action extrusion arrangement enables piercing and extrusion operations to be coordinated, providing the mechanical foundation for manufacturing hollow copper alloy sections with controlled dimensions.
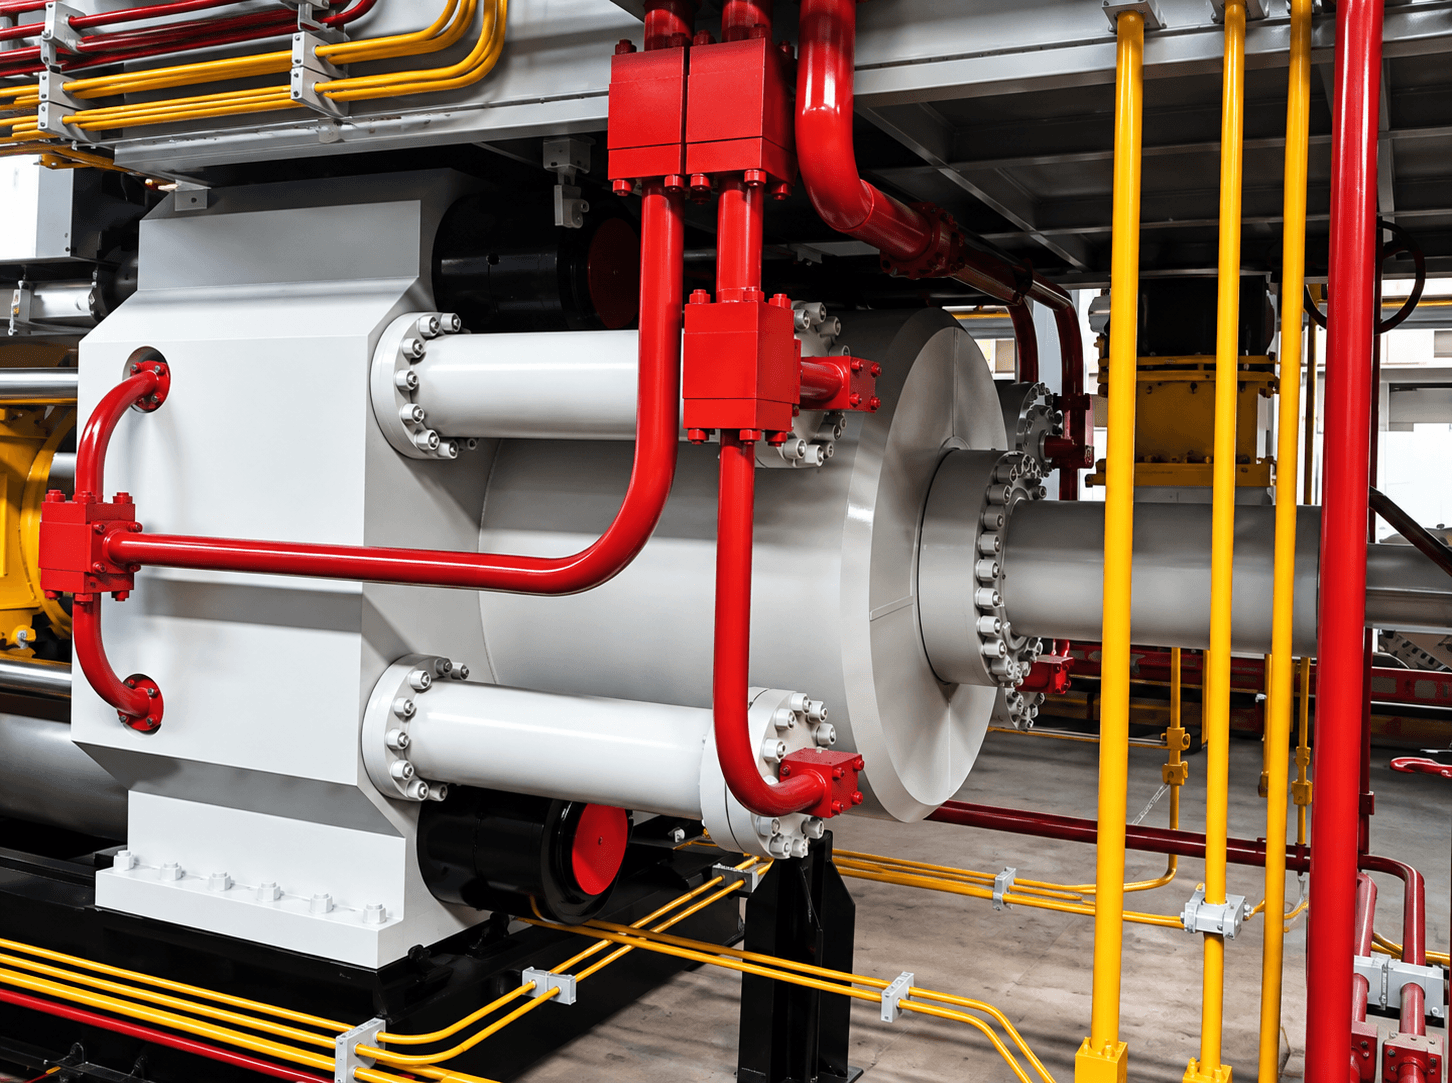
Rated extrusion force 3000 tons, hydraulic working pressure 28 MPa for heavy-duty copper alloy extrusion. Powered by main and auxiliary side cylinders. Adjustable extrusion speed: 0.5–50 mm/s, configurable based on billet, product and tooling conditions.
3D FEA optimized prestressed three-beam four-column frame. Prestressed tie rods and rigid frame minimize deformation under load, keeping extrusion stem, container and die aligned to ensure consistent product dimensions. Preload force is 1.1× maximum extrusion force.
Integrated hydraulic piercing unit produces copper alloy seamless tubes from solid billets. Max piercing force 889 tons, supporting fixed and moving mandrel modes. Guided mandrel maintains alignment for hollow copper alloy products.
Siemens PLC system with 15” touchscreen. Operators set and monitor pressure, speed, stroke, position and container temperature. Auto, semi-auto and manual modes for production, setup and maintenance.
Two-layer structure: H13 inner liner + 5CrNiMo forged steel outer jacket. Electric resistance heating with temperature sensors, max container temperature 500°C. Automatic temperature control for preheating and production.
Servo billet loader, hydraulic pusher and automatic dummy block circulation system. Automates billet positioning and transfer, cuts manual work and enables continuous extrusion cycles.
Immediate water cooling as material exits die. Special water-sealing head prevents backflow into die and container. Water immersion reduces surface oxidation by isolating extruded copper from air.
25 m step-type cooling table with stainless steel / copper contact surfaces to avoid scratches. Equipped with saw conveyor, hydraulic circular saw and discharge system for cooling, conveying, cutting and collection.

Produce seamless copper alloy tubes with stable wall thickness and dimensions for subsequent drawing and machining.

Extrude solid copper alloy rods for further forming and processing.

Custom copper alloy profiles with matched dies for mechanical and electrical applications.

Extrude copper flat sections and busbars as semi-finished materials for power distribution equipment.

Complete extrusion, cooling and cutting line as core equipment for multi-type copper alloy semi-finished goods.

Upstream forming equipment for custom tubes, rods and profiles before precision cutting, drawing and finishing.
|
Parameter |
Specification |
|---|---|
|
Product Name |
Copper Alloy Direct Double-Action Horizontal Extrusion Press |
|
Model |
XJ-3000ZSL |
|
Rated Extrusion Force |
3000 T |
|
Extrusion Method |
Direct / Forward Double-Action Extrusion |
|
Machine Structure |
Prestressed Three-Beam, Four-Column Frame |
|
Hydraulic Working Pressure |
28 MPa |
|
Main Cylinder Diameter |
Φ1120 mm |
|
Main Cylinder Extrusion Force |
2759 T |
|
Maximum Main Stroke |
2200 mm |
|
Adjustable Extrusion Speed |
0.5–50 mm/s |
|
Side Cylinder Extrusion Force |
345 T |
|
Maximum Piercing Force |
889 T |
|
Piercing Cylinder Effective Stroke |
600 mm |
|
Billet Diameter |
Φ250–300 mm |
|
Reference Billet Length for Seamless Tubes |
300–500 mm |
|
Extrusion Container Inner Diameter |
Φ260–315 mm |
|
Extrusion Container Length |
1000 mm |
|
Maximum Container Heating Temperature |
500°C |
|
Die Stack Size |
Φ500 × 500 mm |
|
Extrusion Exit Opening |
Φ350 mm |
|
Control System |
Siemens PLC + 15-Inch Touchscreen |
|
Operation Modes |
Automatic / Semi-Automatic / Manual |
|
Water-Sealing System Length |
28 m |
|
Step-Type Cooling Table |
25 × 3.5 m |
|
Saw-Cut Transfer Conveyor Length |
25 m |
The 3000T copper alloy extrusion line combines the following main equipment and process systems.
The central hydraulic machine provides extrusion force through its prestressed frame, main working cylinder, side cylinders, extrusion beam and container assembly.
The integrated mandrel and piercing cylinder support seamless-tube extrusion, with controlled mandrel movement and alignment during production.
A servo-driven loading mechanism positions heated billets for transfer into the extrusion press, reducing manual handling during repeated production cycles.
A hydraulic pusher transfers billets into the loading mechanism. Position detection and length measurement support coordinated billet feeding.
The heated container, die slide and hydraulic locking devices hold and position the tooling required for copper alloy extrusion.
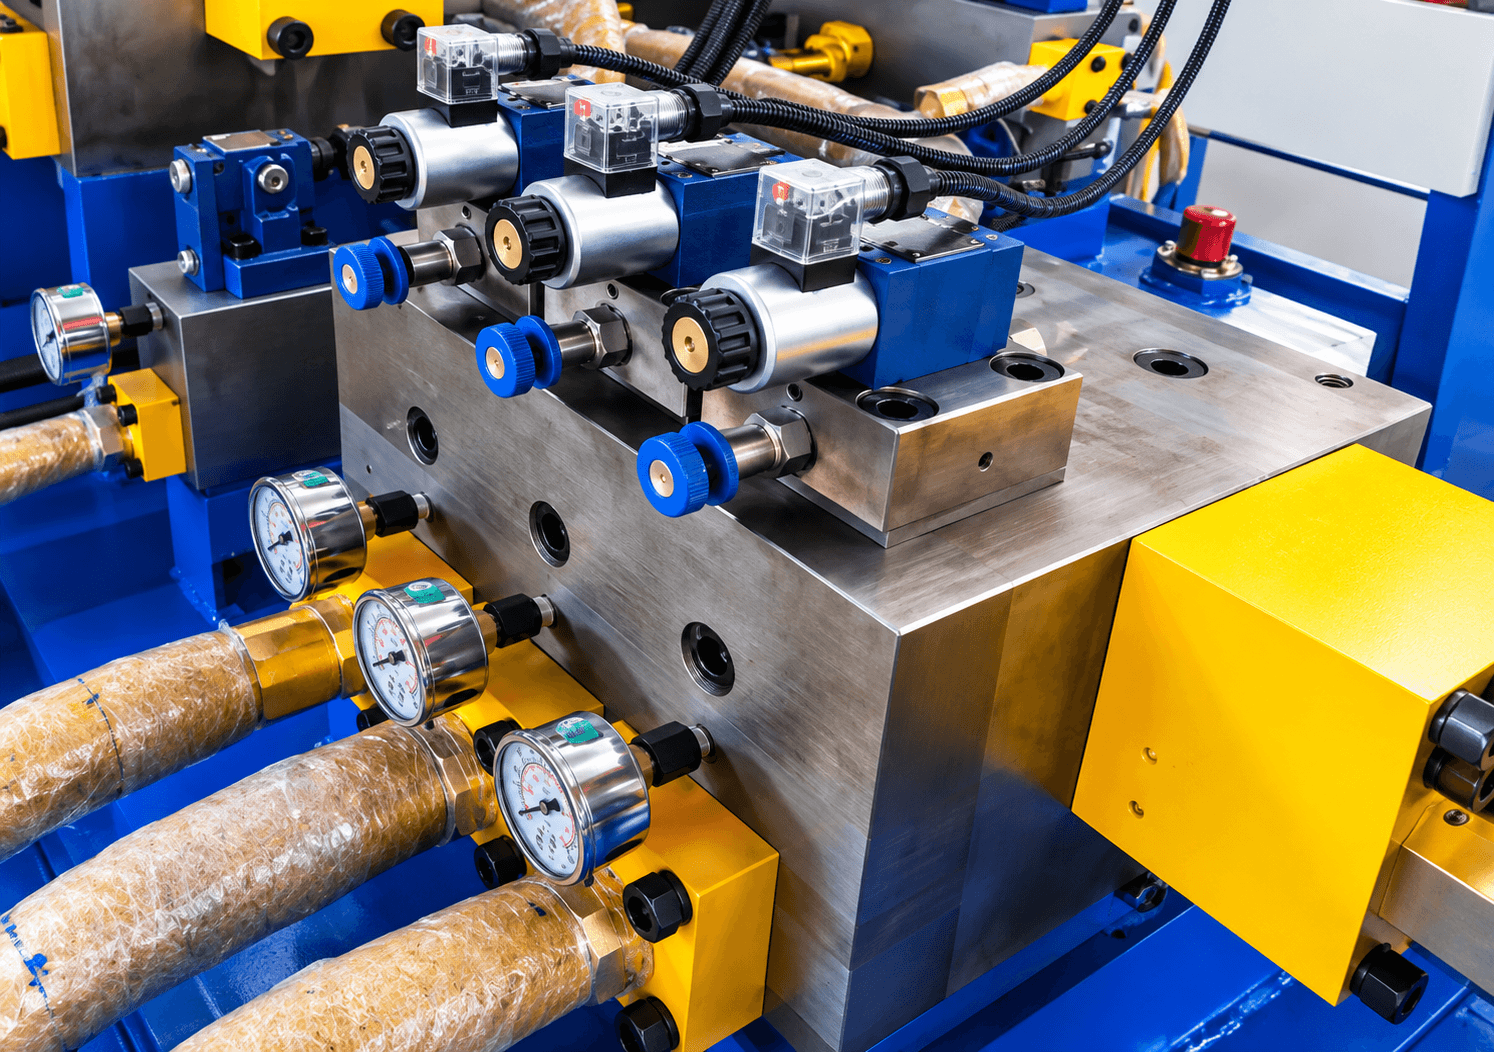
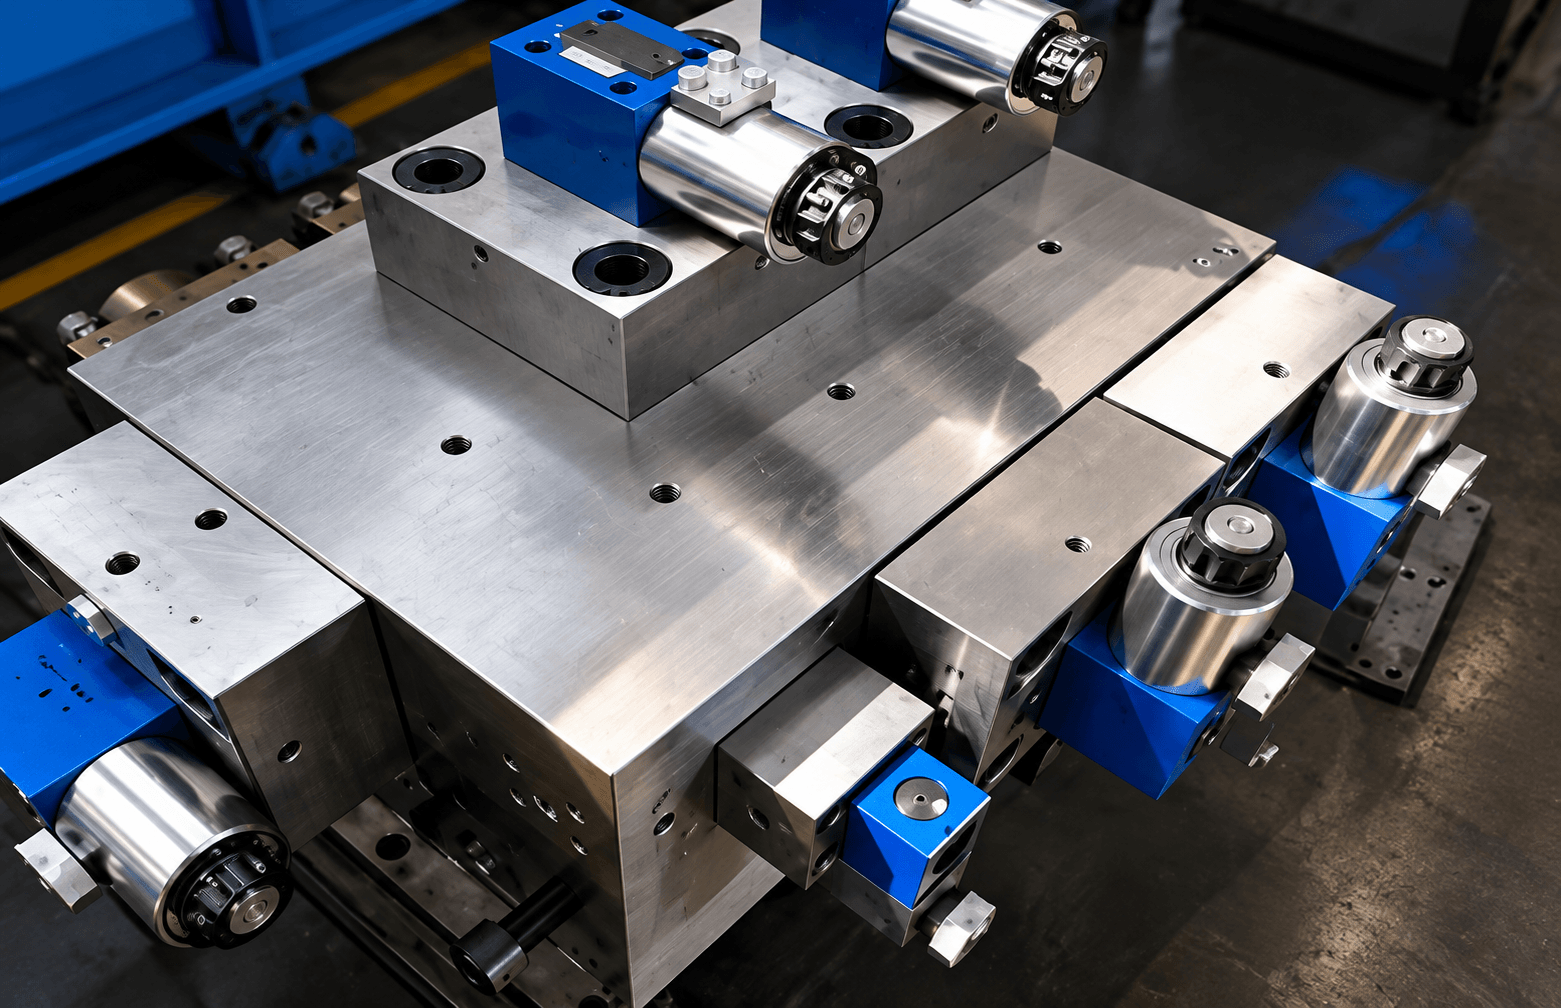
The hydraulic equipment incorporates high-pressure pumps, valves, filtration, oil cooling and pressure-monitoring components to coordinate press movements and extrusion operations.

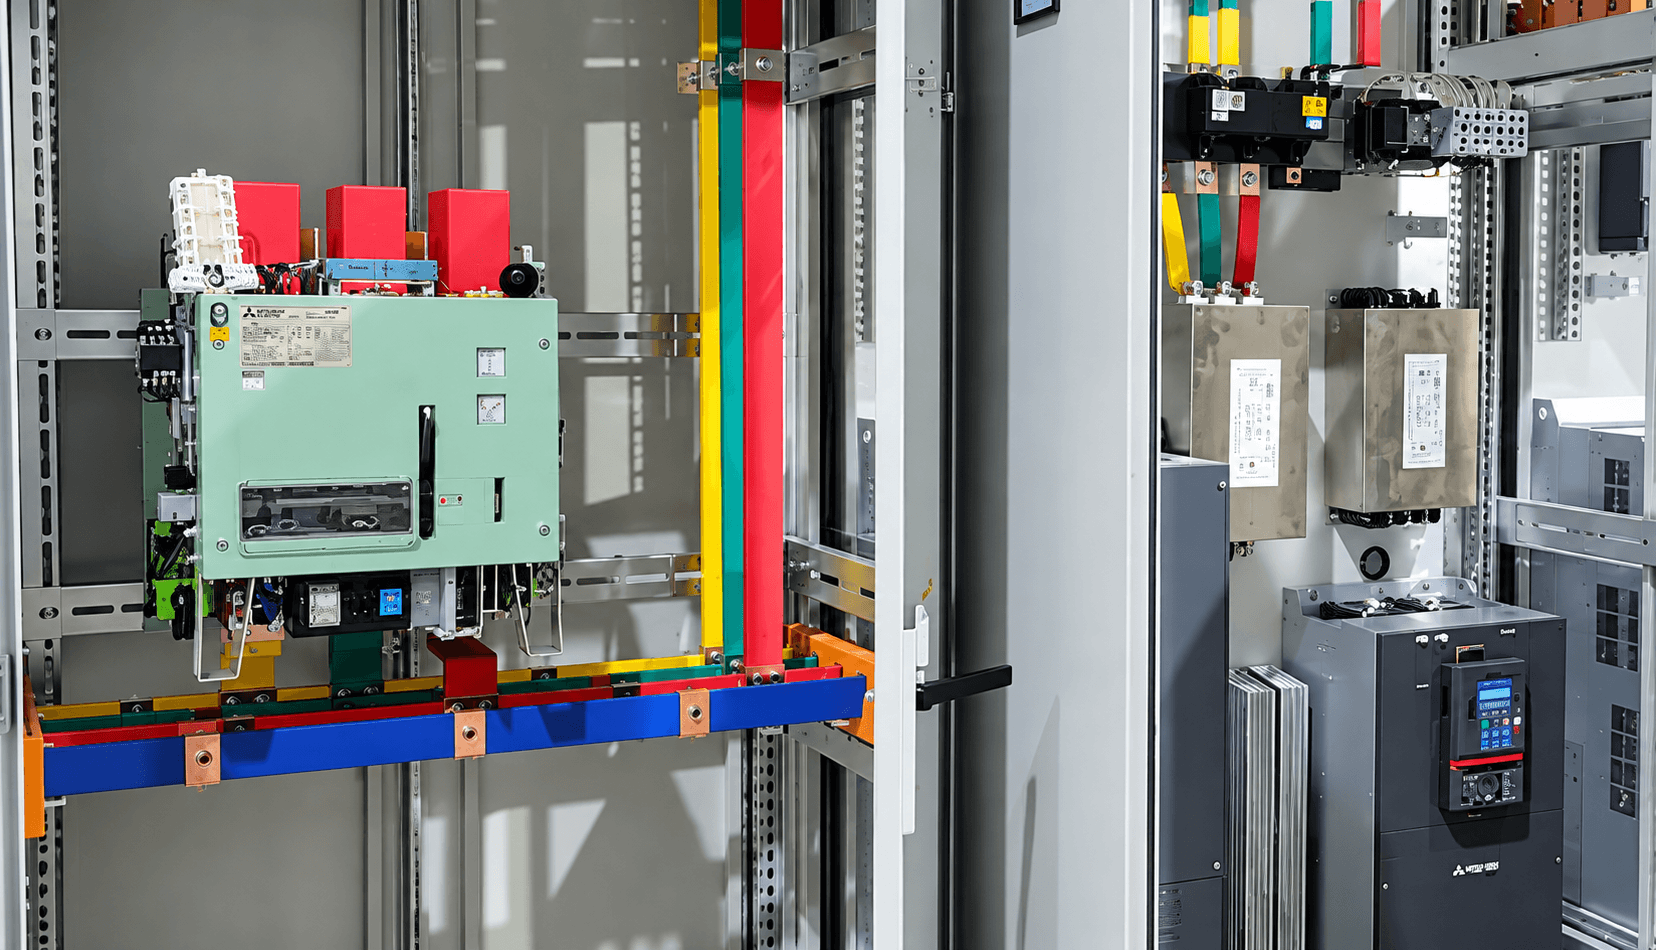
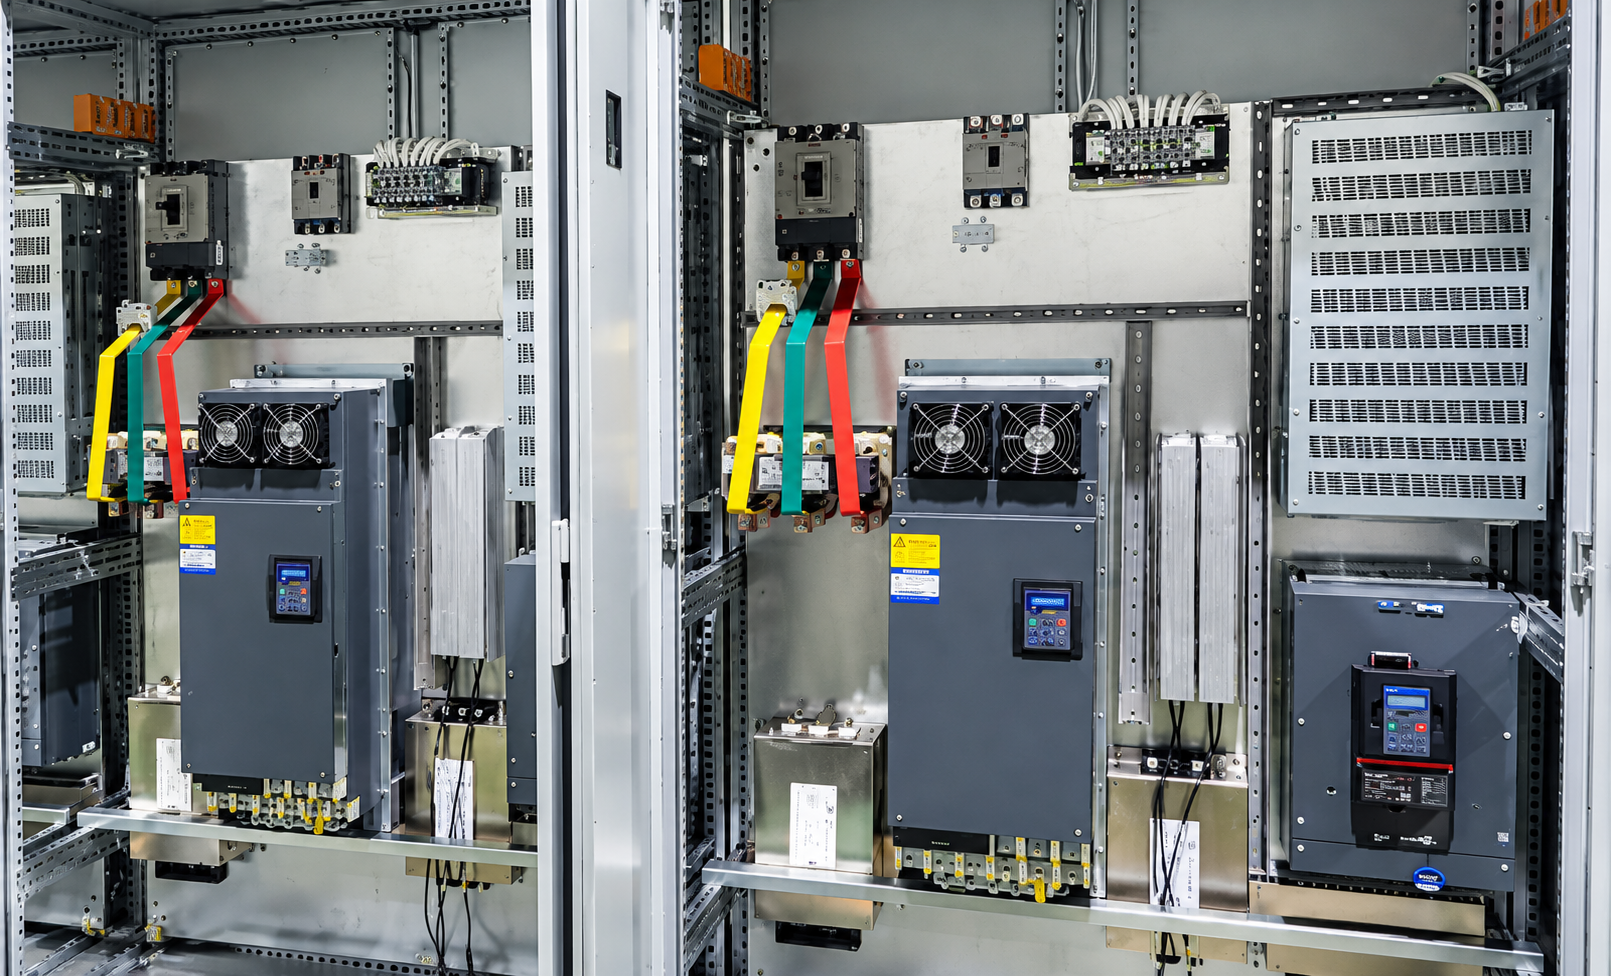
The electrical system includes control cabinets, Siemens PLC automation, a touchscreen interface, sensors, switches and associated control components.

The mechanism collects and transfers movable dummy blocks after extrusion and returns them to the preparation position for subsequent cycles.
The downstream water-sealing equipment includes a sealing head, transition channel, water trough, product transfer mechanism and water pump station.
The cooling table uses fixed and moving support arms to advance extruded copper products through the handling section.
The cutting section includes a 25 m transfer roller conveyor, hydraulic circular saw and product clamping mechanism for cutting extruded materials to specified lengths.
A 7 m output roller table, adjustable length-setting mechanism and receiving rack provide downstream product handling after cutting.
| Equipment | Reference Specification |
|---|---|
| Processing Material | Copper and Copper Alloys |
| Product Types | Seamless Tubes, Rods, Profiles, Busbars |
| Seamless Tube Outer Diameter | Φ60–200 mm |
| Seamless Tube Inner Diameter | Φ50–150 mm |
| Seamless Tube Wall Thickness | ≥5 mm |
| Rod Diameter | Φ10–80 mm |
| Seamless Tube Wall Thickness Deviation | Maximum ≤10% of Average Wall Thickness |
| Profile Dimensional Acceptance Reference | GB/T 14846-2008 |
A complete copper alloy extrusion line requires more than extrusion force alone. Billet preparation, tooling alignment, hydraulic motion, cooling, cutting and material transfer must operate as a coordinated process.
The XJ-3000ZSL extrusion system is designed around this integrated production approach.
Copper alloy billets are prepared to the required dimensions and extrusion temperature before entering the loading system.
The billet loading mechanism and hydraulic pusher position the billet for transfer into the extrusion container.
The extrusion container is heated to the selected operating temperature, while the appropriate die and mandrel configuration are prepared.
The main hydraulic cylinder provides extrusion force. For seamless-tube production, the integrated piercing system coordinates the mandrel and extrusion movement.
The extruded product exits the die and enters the water-sealing system for controlled cooling and reduced atmospheric exposure.
The cooled product moves along the step-type handling table toward the cutting area.
The saw-cut transfer conveyor moves the product to the hydraulic circular saw for cutting to the required length.
Cut products are transferred to the output table and receiving rack for inspection, subsequent processing or storage.
Every copper alloy extrusion project has different requirements for product dimensions, alloy composition, production capacity, workshop arrangement and downstream processing.
PINMI can coordinate the technical configuration of the 3000T horizontal copper alloy extrusion press line according to the buyer's production objectives.
Project engineering considerations include:

Copper Alloy Grade

Finished Product Dimensions

Billet Specifications

Extrusion Tooling
Cooling and Handling
Automation Requirements
Workshop and Utilities
Installation and Commissioning
Check our FAQs below, or reach out to our team for tailored answers and project quotation.
Get a Quote
Share your capacity, raw material and site conditions — we'll come back with a process route, equipment selection and a turnkey path to production.


No.310–311 National Road, Quanshan District, Xuzhou City, China