Pinmi
Get a Quote
Pinmi
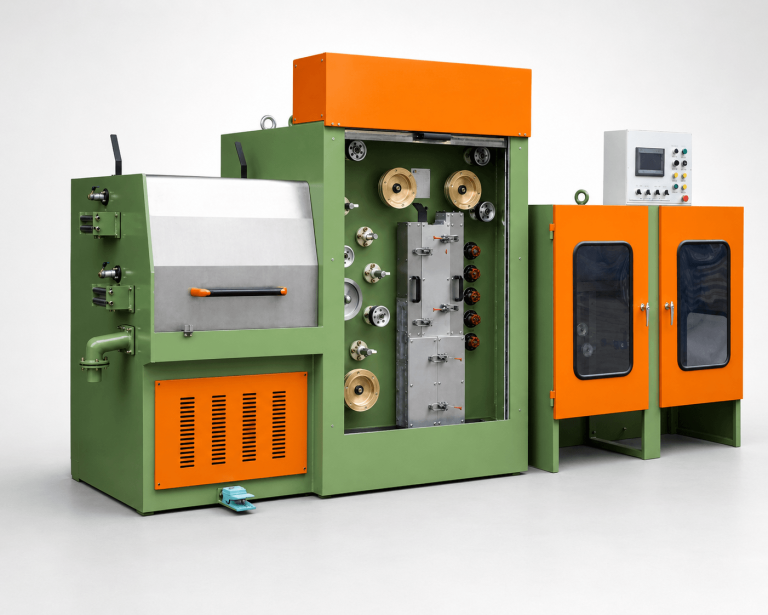
Each drawing capstan is independently driven, and the drawing speed can be synchronized and adjusted through the control system. This helps maintain stable drawing conditions across multiple passes.
The single-line capstan arrangement, detachable double-taper capstan rings and smooth wire route reduce wire shaking and surface friction. This helps improve the surface quality of aluminum wire.
Pneumatic tension control, wire-break detection, stable take-up and reasonable wire path help reduce wire vibration and breakage during high-speed production.
The machine supports up to 25 m/s outlet speed and automatic double-spool take-up. When the preset length is reached, the system switches from full spool to empty spool to support continuous production.
A 13-pass drawing process and adjustable elongation setting allow the machine to match different die schedules and outlet wire diameters for cable and conductor production.

Power Cable Production

Electrical Conductor Manufacturing

Aluminum Wire Processing

Overhead Conductor Production
Building Wire and Cable Industry
Industrial Aluminum Wire Production
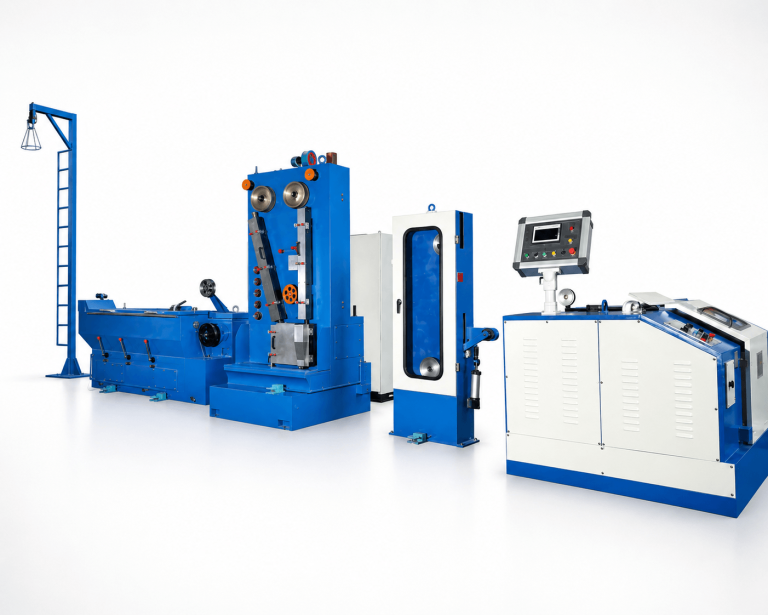
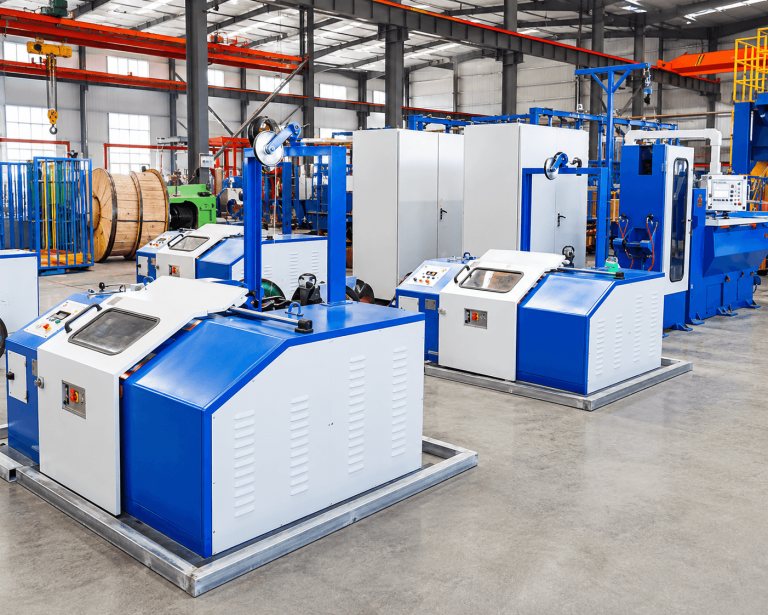
The system is delivered as a sequence of coordinated stations, each built and tested in-house before shipment.

Double‑position swing‑arm pay‑off stand feeds Φ9.5/12 mm aluminum rod, equipped with anti‑disorder‑wire and emergency‑stop devices.

LFDL‑450/13 drawing host with Φ450 mm capstans, 13 drawing passes and independent servo‑motor drive for each capstan.

Provides spray cooling & circulating lubrication for drawing dies and capstans to guarantee high‑speed drawing condition.

Pneumatic tension control with wire‑break detection and electronic metering, keeps stable tension during whole drawing procedure.

Optional automatic double‑spool take‑up or basket coiler, supports auto spool switching for non‑stop production.

- Siemens PLC + HMI centralized control, with fault alarm, remote communication and full‑range safety interlock functions.
Reference size cover most projects. Intermediate capacities and custom configurations are engineered on request.
| Item | Specification |
| Machine Model | LFDL-450/13 equal-diameter separate-motor aluminium large wire drawing machine |
| Application | Drawing aluminum rod or aluminum alloy rod into round aluminum / aluminum alloy single wire |
| Inlet Wire Diameter | Φ9.5 mm / Φ12 mm |
| Inlet Rod Tensile Strength | <=160 MPa |
| Outlet Wire Diameter | Φ1.78-Φ4.2 mm from Φ9.5 mm rod; Φ2.25-Φ4.2 mm from Φ12 mm rod |
| Wire Material | Aluminum rod, heat-resistant aluminum alloy rod, aluminum alloy wire material according to process requirements |
| Drawing Speed | Maximum 25 m/s when outlet wire diameter is Φ1.78 mm |
| Number of Drawing Dies | Maximum 13 passes |
| Capstan Diameter | Φ450 mm drawing capstan |
| Drawing Motor Power | 12 x 30 kW AC servo motors + 1 x 75 kW AC servo motor |
| Double-Spool Take-up Motor | 2 x 30 kW AC servo motors |
| Basket Coiler Motor | 15 kW AC servo motor |
| Traverse Motor | 2.2 kW AC servo motor for double-spool take-up; 0.2 kW AC for basket coiler traverse |
| Storage Length | 6 m accumulator storage length |
| Take-up Type | Automatic double-spool take-up and basket coiler |
| Take-up Bobbin | PND630 / PND500; double-spool take-up supports PND630 / PND560 |
| Basket Coiler Size | Φ600 x Φ1100 x H1950 mm |
| Basket Coiler Max Loading | 2000 kg |
| Maximum Take-up Speed | 25 m/s when outlet wire diameter is Φ1.78 mm |
| Maximum Traverse Pitch | 10 mm |
| Tension Control | Pneumatic tension control, max tension 250 N |
| Metering Accuracy | ±3‰ |
| Lubrication Method | Spray lubrication and circulating cooling for drawing dies; semi-immersed circulating cooling for drawing capstans |
| Wire Pointer / Threading Machine | Rolling range 1.78-12 mm; rolling roller diameter 100 mm; roller speed 24 r/min; capstan diameter 430 mm; main motor 5.5 kW AC |
| Control System | PLC and touch screen centralized control; Siemens PLC and Siemens HMI in documented configuration |
| AC Drive | Danfoss AC drives in documented configuration |
| Low-Voltage Electrical Components | Schneider components in documented configuration |
| Power Supply | Three-phase five-wire system, 380 V ±10%, 50 Hz; single-phase control voltage 220 V |
| Installed Power | 523 kW |
| Compressed Air Requirement | 0.6 MPa, 0.4 m3/min; dry and clean compressed air required |
| Cooling Water Requirement | 0.3 MPa, 0.2 m3/min |
| Noise Level | <=85 dB |
| Operating Environment | Temperature 0-40 deg C; humidity 5%-90% |
| Machine Layout | Right-hand or left-hand operation available according to project layout |
| Customization Available | Inlet/outlet diameter, die schedule, capstan configuration, take-up type, control components, voltage, line layout and complete production line matching |
Reference values — final parameters are confirmed during process design based on raw material, site conditions and product standard. Replace with your confirmed datasheet values before publishing.
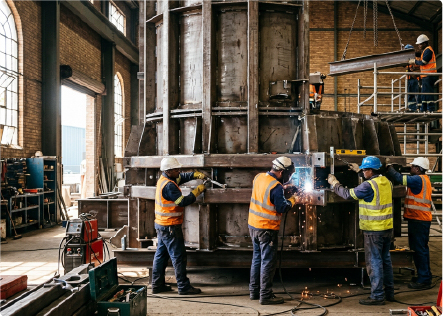
workshop
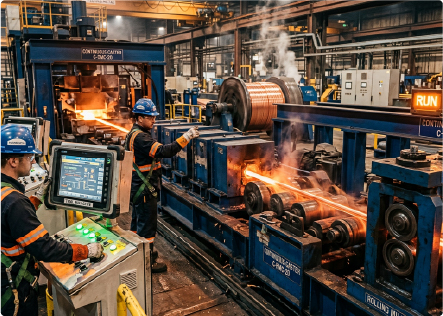
trial run
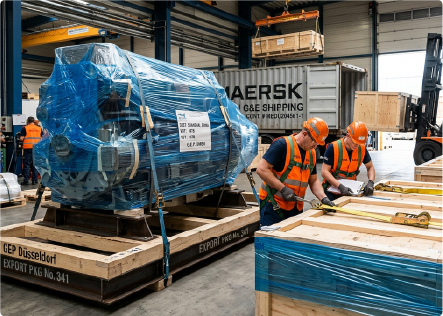
container load
workshop
Share your capacity, raw material and site conditions — we'll come back with a process route, equipment selection and a turnkey path to production.


No.310–311 National Road, Quanshan District, Xuzhou City, China
Check our FAQs below, or reach out to our team for tailored answers and project quotation.
Get a Quote